Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier specializing in the production of organic fertilizer granules and related processing equipment. Based in Shandong, China, the company has established itself as a key player in the agricultural machinery sector, focusing on delivering high-quality solutions for organic fertilizer production. This article provides an in-depth overview of the technical parameters and the conveying system process used in the organic fertilizer granules production line, highlighting the efficiency and precision of the equipment designed by HeadPowder.
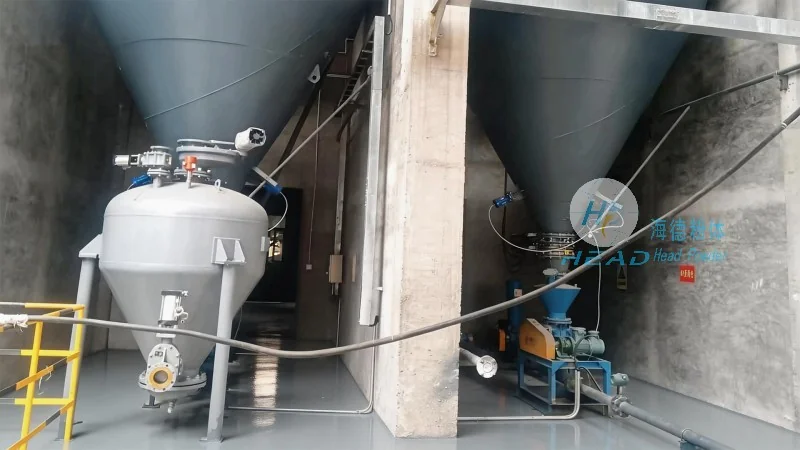
Key Technical Parameters for Organic Fertilizer Granules Production
The technical parameters of the organic fertilizer granules production system are crucial for ensuring the quality and consistency of the final product. These parameters are meticulously designed to meet industry standards and customer requirements. The granulation process involves several critical factors, including moisture content, particle size distribution, and granule strength. The moisture content of the raw materials is typically maintained between 12% to 15% to facilitate the granulation process. The particle size of the final granules is usually controlled within a range of 2 to 5 millimeters, with a target bulk density of 0.8 to 1.2 g/cm³. Granule strength is assessed through compressive strength tests, with a minimum requirement of 10 N per granule to ensure durability during handling and transportation.
Additionally, the system incorporates advanced sensors and control mechanisms to monitor and adjust these parameters in real-time. For instance, the moisture content is continuously measured using in-line moisture sensors, and the conveyor speed is automatically adjusted based on the measured values to maintain optimal conditions. The particle size is controlled by adjusting the rotation speed of the granulation drum and the size of the screen used for classification. The granule strength is evaluated through automated testing equipment that samples a representative batch and measures the force required to break the granules. These technical parameters are not only essential for product quality but also contribute to the overall efficiency of the production process, reducing waste and improving yield.
The Conveying System Process in Organic Fertilizer Granules Production
The conveying system is a vital component of the organic fertilizer granules production line, responsible for transporting raw materials, intermediate products, and finished granules through various stages of the process. HeadPowder's conveying system is designed with a focus on reliability, energy efficiency, and minimal product degradation. The system typically consists of a combination of screw conveyors, belt conveyors, and pneumatic conveyors, each serving a specific function in the production workflow.
Raw materials such as compost, manure, and other organic substances are first fed into the system via a hopper. From there, they are transported to the mixing and pre-treatment stage using a screw conveyor. The screw conveyor is equipped with a variable speed drive, allowing for precise control over the material flow rate. This ensures that the raw materials are mixed uniformly and that the moisture content is adjusted as needed before granulation.
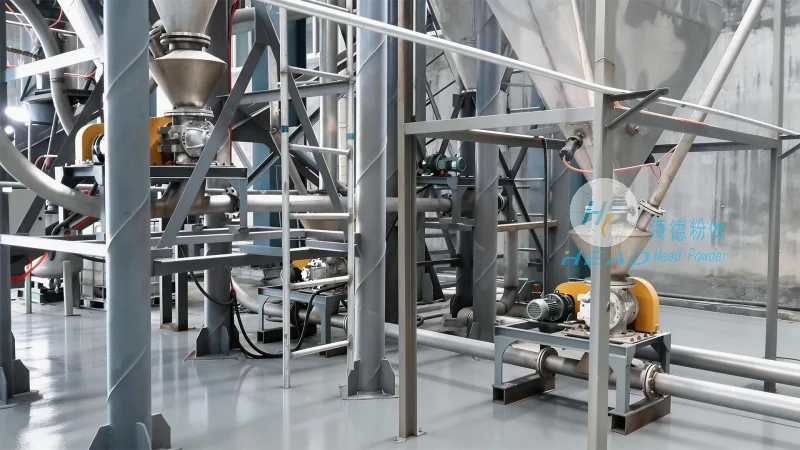
After the mixing stage, the materials are conveyed to the granulation unit. The granulation process involves the use of a rotating drum where the materials are agitated and compacted into granules. The conveying system from the granulation drum to the screening and classification unit is typically handled by a belt conveyor. This conveyor is designed with a smooth surface to prevent granule breakage and is equipped with adjustable speed controls to match the output of the granulation unit.
The screened granules are then transported to the drying and cooling stage. A pneumatic conveying system is often used for this purpose, as it allows for efficient and dust-free transportation of the granules. The pneumatic system uses air pressure to move the granules through a pipeline, ensuring that the product remains intact and free from contamination. The conveying velocity is carefully controlled to prevent granule attrition and to maintain the desired moisture content after drying.
Once the granules are dried and cooled, they are conveyed to the packaging unit. A belt conveyor is commonly used for this final stage, transporting the finished granules into the packaging machine. The conveying speed is synchronized with the packaging speed to ensure a smooth and continuous operation. The system also includes a dust collection and filtration unit to maintain a clean working environment and to comply with environmental regulations.
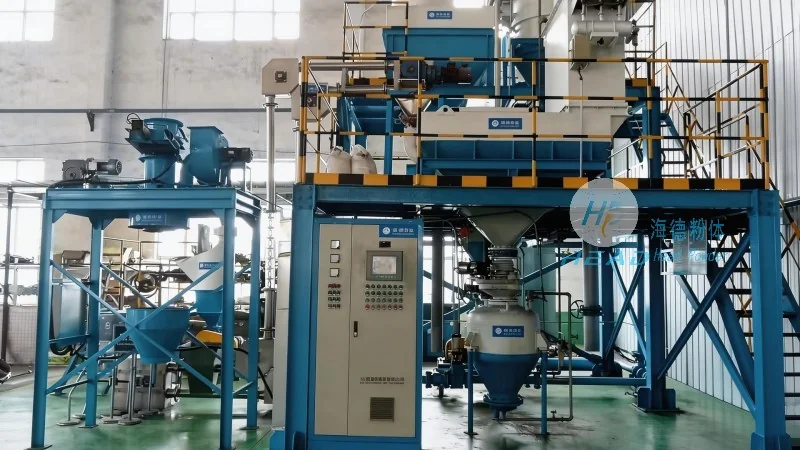
Efficiency and Advantages of the Conveying System
The conveying system designed by Shandong HeadPowder Engineering Co., Ltd. offers several advantages over traditional methods. One of the key benefits is the reduction in labor costs, as the system automates the material handling process, minimizing the need for manual intervention. This not only improves operational efficiency but also enhances workplace safety by reducing the risk of accidents associated with manual material handling.
Another advantage is the improved product quality and consistency. The automated conveying system ensures that the materials are transported uniformly and at a controlled speed, preventing over-processing or under-processing of the granules. This leads to a more consistent product with uniform moisture content and particle size, which is crucial for the effectiveness of the organic fertilizer. The system also reduces product loss and waste, as the conveyor design minimizes spillage and material degradation.
Energy efficiency is another significant advantage of the conveying system. The use of variable speed drives and energy-saving motors reduces the overall energy consumption of the system, contributing to lower operational costs and a smaller environmental footprint. The system is also designed for easy maintenance and repair, with accessible components and clear operational indicators, ensuring minimal downtime and maximum productivity.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides comprehensive solutions for organic fertilizer granules production, with a focus on advanced technical parameters and an efficient conveying system. The company's expertise in designing and manufacturing high-quality equipment ensures that customers receive reliable and effective solutions that meet their specific needs. By adhering to strict quality control measures and continuous innovation, HeadPowder remains committed to delivering superior products and services to the agricultural industry. The technical parameters and conveying system process outlined in this article demonstrate the company's dedication to excellence and its role as a leader in the organic fertilizer granules production sector.




