HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. The company's expertise lies in pneumatic conveying systems, which are crucial for efficient transport of aggregates like sand and gravel in various industrial applications.
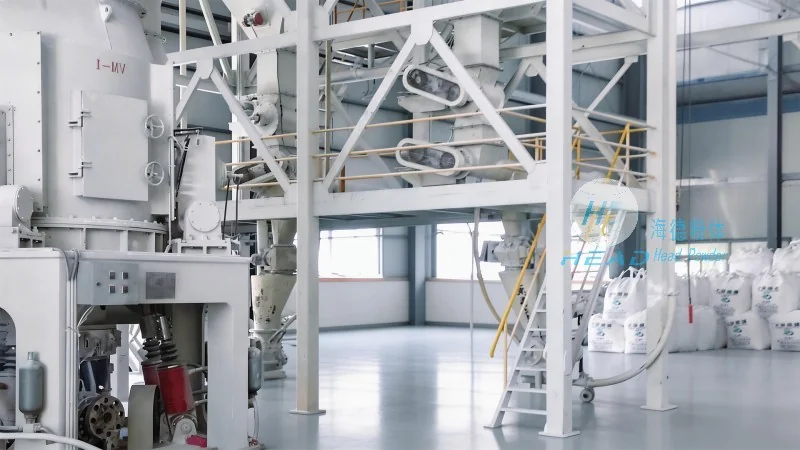
Types of Pneumatic Conveying Systems for Aggregate Transport
There are primarily two types of pneumatic conveying systems used in the transport of aggregates: positive pressure and negative pressure systems. Positive pressure systems operate by blowing air or gas into the material to move it through a pipeline. This method is suitable for long-distance transport and can handle a wide range of materials, including fine powders and bulk solids. Negative pressure systems, on the other hand, use suction to draw material into the pipeline, making them ideal for applications where dust control is a priority and the material is light and easily airborne.
Practical Applications in Aggregate Transport
HeadPowder's pneumatic conveying systems are widely applied in the construction industry, particularly in concrete production facilities. In these settings, the systems efficiently transport sand, gravel, and other aggregates from storage silos to mixing plants, ensuring a continuous and controlled supply of raw materials. The technology also finds use in mining operations, where it helps in the transport of crushed rock and ore from processing plants to storage or further processing units. Additionally, in recycling and waste management facilities, pneumatic conveying systems are employed to handle recycled aggregates, facilitating the circular economy by optimizing material recovery and reuse.
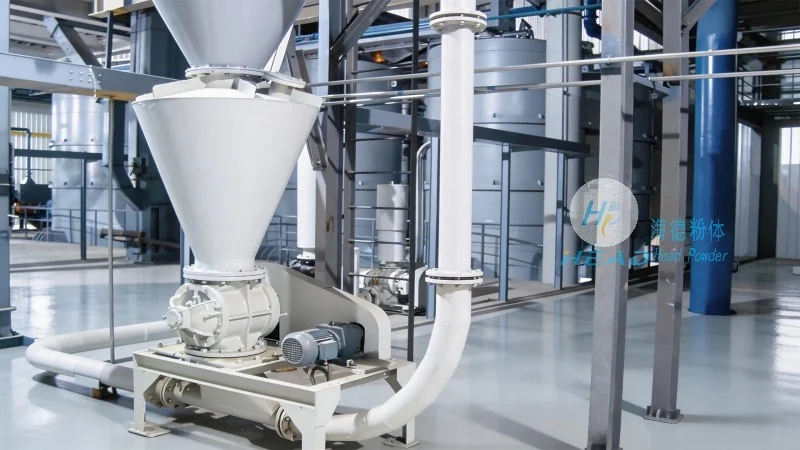
Key Advantages of Pneumatic Conveying Systems
Compared to traditional mechanical conveyors, pneumatic systems offer several advantages in aggregate transport. They provide a dust-free and enclosed transport environment, which is essential for maintaining air quality and worker safety. The systems are also flexible in layout, allowing for complex routing and integration with existing plant infrastructure. Furthermore, pneumatic conveying can handle materials with varying moisture content and particle sizes without the risk of blockages or wear that may occur with mechanical systems. These benefits make pneumatic conveying a preferred choice for high-volume and high-purity aggregate transport applications.
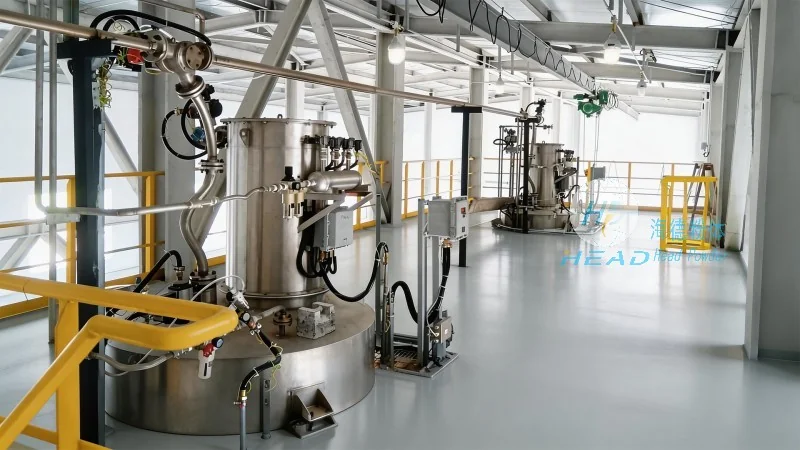
Customization and Integration Services
HeadPowder offers customized pneumatic conveying solutions tailored to specific project requirements. The company works closely with clients to assess site conditions, material characteristics, and operational needs to design systems that meet performance, efficiency, and safety standards. Integration services include the installation of silos, hoppers, and control panels, as well as the provision of maintenance and support services to ensure long-term system reliability. By leveraging advanced engineering and manufacturing capabilities, HeadPowder ensures that its pneumatic conveying systems deliver optimal performance and contribute to the overall productivity of aggregate handling operations.
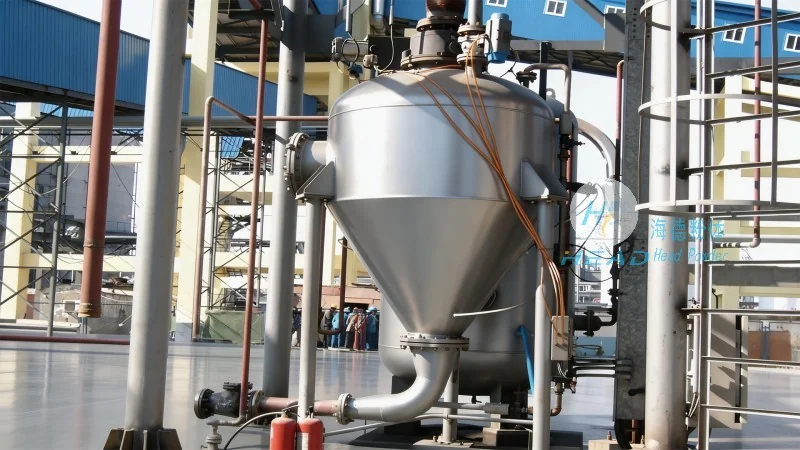
Case Study: Concrete Production Plant in Shandong
A recent project for a large concrete production plant in Shandong involved the installation of a positive pressure pneumatic conveying system to transport sand and gravel from on-site storage to the mixing area. The system, designed by HeadPowder, consisted of a series of pipelines, airlocks, and control units that ensured a steady flow of materials. The implementation resulted in a significant reduction in material handling time and labor costs, while maintaining strict dust control measures. The client reported improved operational efficiency and compliance with environmental regulations, highlighting the effectiveness of HeadPowder's pneumatic conveying solutions in real-world applications.
Future Trends and Innovations
As the construction and mining industries continue to evolve, pneumatic conveying systems are expected to incorporate advanced technologies to enhance performance and sustainability. HeadPowder is at the forefront of these innovations, exploring the integration of automation, IoT sensors, and energy-efficient air compressors into its systems. These advancements aim to further reduce operational costs, improve material handling accuracy, and minimize environmental impact. By staying committed to research and development, HeadPowder ensures that its pneumatic conveying solutions remain cutting-edge and capable of meeting the future demands of aggregate transport.




