

Design of Pneumatic Conveying System for Feather Handling
Feather processing operations demand specialized material handling solutions to maintain efficiency and product integrity. The pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. is specifically tailored to meet the unique challenges of handling feather materials. This system leverages advanced engineering principles to ensure reliable transport of feathers from collection points to processing facilities, while minimizing operational disruptions and product degradation.
Key Features of the Pneumatic Conveying System
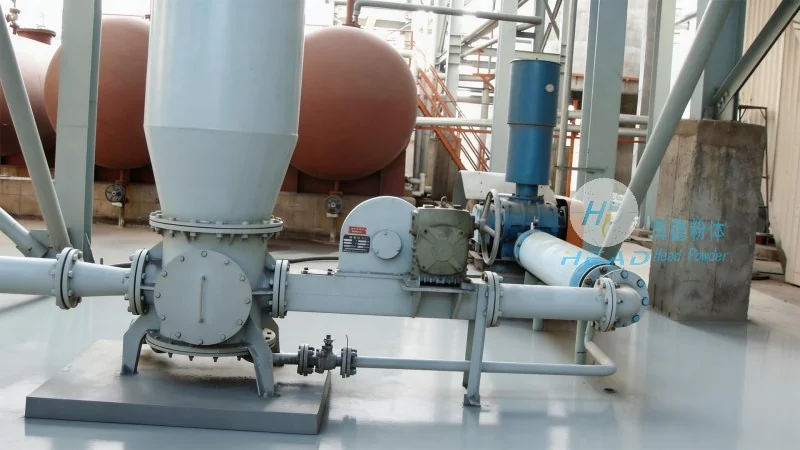
The pneumatic conveying system for feather handling incorporates several key features that enhance its performance and adaptability. These include high-capacity air flow management, adjustable pressure control, and specialized hopper designs to accommodate the light and irregular nature of feathers. The system is equipped with durable components that resist wear and tear from continuous operation, ensuring long-term reliability. Additionally, the design incorporates safety features to prevent material blockages and maintain consistent airflow, which is critical for maintaining system efficiency.
System Components and Operational Principle
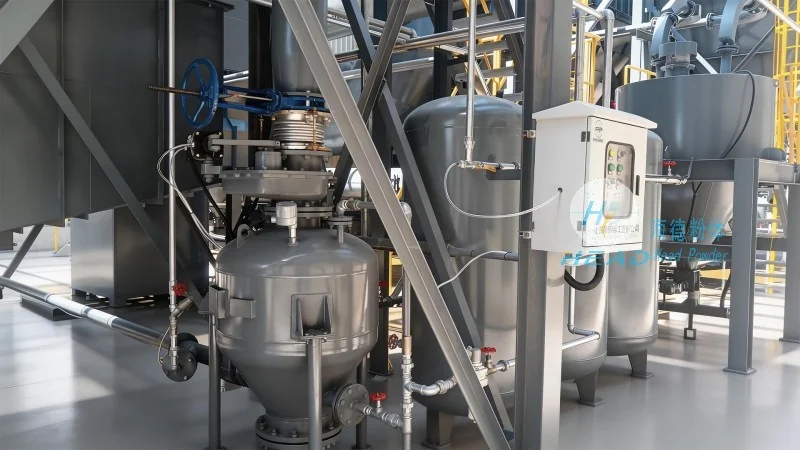
The pneumatic conveying system consists of several core components, each playing a vital role in the material transport process. The system includes a hopper for material storage, a rotary valve for controlled material discharge, a pipeline network for air and material transport, and a receiver for product collection. The operational principle involves using compressed air to create a flow that carries the feather particles through the pipeline. The air flow is carefully regulated to ensure that the feathers are conveyed without excessive pressure or turbulence, which could damage the delicate structures of the feathers. The system also features a filtration system to remove any dust or debris from the air, maintaining air quality and system longevity.
Advantages of the Pneumatic Conveying System
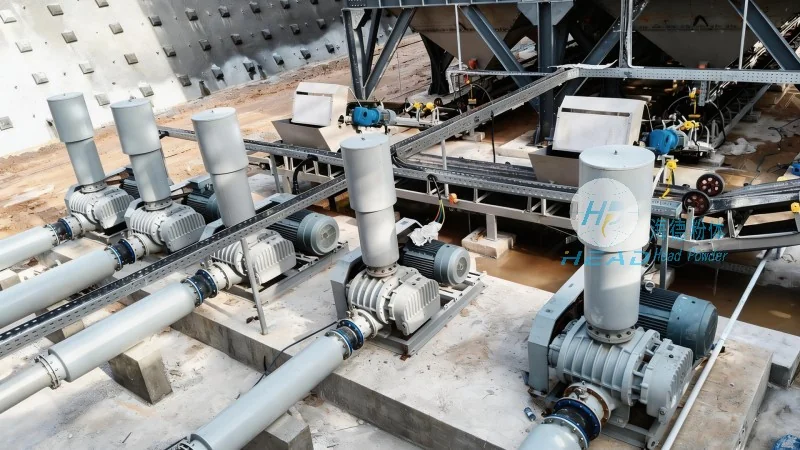
Implementing a pneumatic conveying system for feather handling offers numerous advantages over traditional material handling methods. One of the primary benefits is the ability to transport feathers over long distances with minimal manual intervention. The system reduces labor costs and improves operational efficiency by automating the material transport process. Additionally, the enclosed pipeline system prevents contamination from external sources, ensuring that the feathers remain clean and free from dust or other impurities. The system also minimizes product damage, as the gentle air flow and controlled pressure prevent breakage or loss of feather quality. This results in higher product yields and better market value for the processed feathers.
Customization and Scalability
Shandong HeadPowder Engineering Co., Ltd. offers customized solutions to meet the specific requirements of different feather processing facilities. The pneumatic conveying system can be scaled to accommodate varying production capacities, from small-scale operations to large industrial facilities. The system can be integrated with existing processing equipment, allowing for seamless integration into current production lines. Additionally, the company provides technical support and maintenance services to ensure that the system operates at optimal performance levels. This customization and scalability make the pneumatic conveying system a versatile solution for a wide range of feather processing applications.
Conclusion
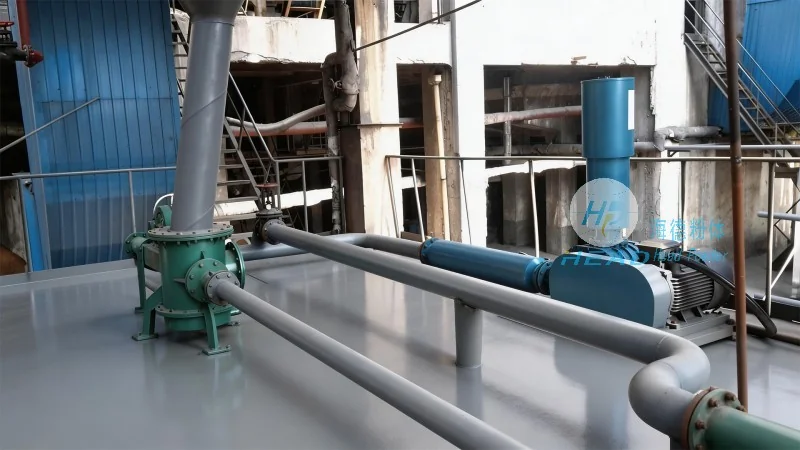
The pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. represents a significant advancement in feather material handling technology. By combining advanced engineering with practical design, the system provides an efficient, reliable, and cost-effective solution for transporting feather materials. The system's ability to handle the unique characteristics of feathers while maintaining high performance makes it an ideal choice for feather processing operations. With its customization options and long-term reliability, the system is well-suited to meet the evolving needs of the feather processing industry.