Phosphate fertilizer powder is a critical raw material in modern agriculture, and efficient handling of this material is essential for maintaining production efficiency and product quality. The traditional methods of transporting phosphate powder, such as manual handling or mechanical conveyors, often face challenges like dust pollution, material loss, and operational inefficiencies. To address these issues, advanced pneumatic conveying systems have emerged as a reliable solution. This article introduces the comprehensive solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, focusing on the technical aspects, benefits, and practical applications of phosphate powder pneumatic conveying systems.
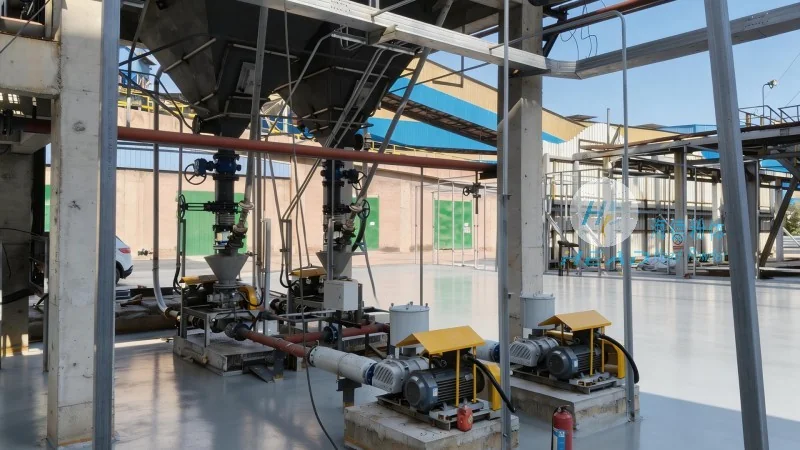
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the abbreviation for Shandong HeadPowder Engineering Co., Ltd., is a professional engineering company based in Shandong, China. With years of experience in the design, manufacturing, and installation of pneumatic conveying systems, HeadPowder specializes in providing customized solutions for various powder handling applications, including phosphate fertilizer powder. The company combines advanced technology with professional engineering expertise to deliver high-performance, reliable, and cost-effective conveying systems that meet the specific needs of clients in the agricultural and chemical industries.
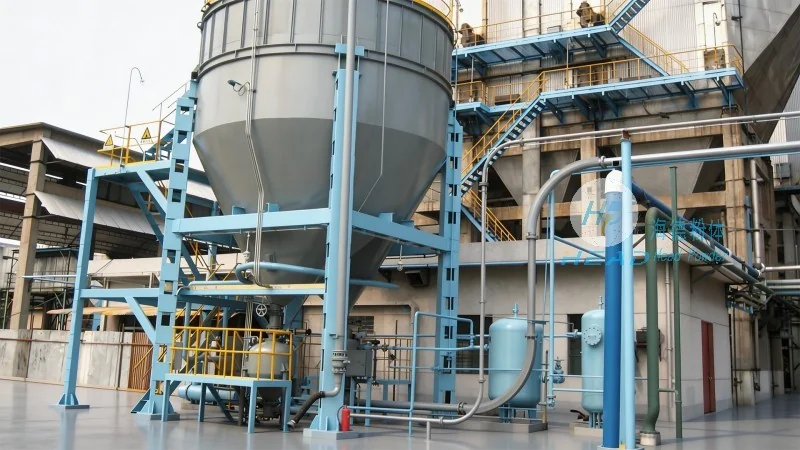
Key Features of Phosphate Powder Pneumatic Conveying Systems
The pneumatic conveying systems for phosphate powder offered by HeadPowder are designed with several key features that enhance performance and reliability. First, the systems utilize positive pressure or negative pressure conveying methods to transport phosphate powder from storage silos to processing units or packaging lines. This method effectively prevents dust leakage and ensures a clean working environment. Second, the equipment is equipped with high-quality materials, such as stainless steel or special alloys, to resist corrosion and wear caused by the abrasive nature of phosphate powder. Third, the systems incorporate advanced control systems that allow for precise flow control, pressure monitoring, and automatic operation, reducing the need for manual intervention and improving operational safety. Additionally, the design of the conveying lines and components is optimized to minimize pressure drops and energy consumption, making the systems energy-efficient and cost-effective.
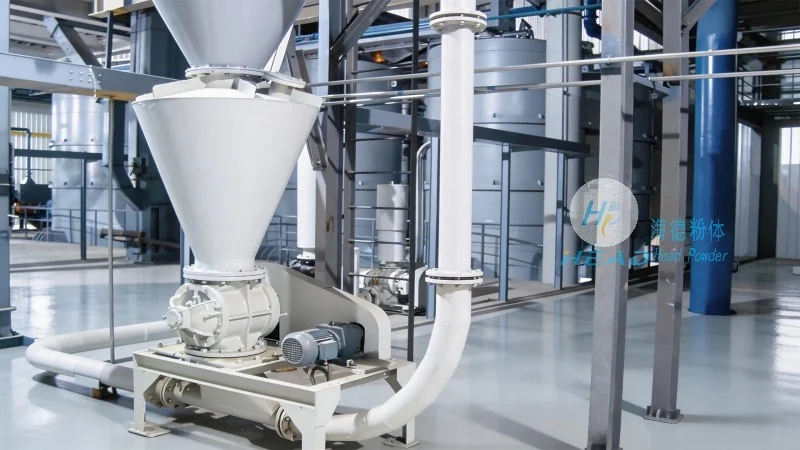
Benefits of Implementing Phosphate Powder Pneumatic Conveying Solutions
Adopting phosphate powder pneumatic conveying solutions from HeadPowder brings numerous benefits to agricultural and chemical companies. One of the primary advantages is the significant reduction in dust pollution, which not only improves the working environment for employees but also complies with environmental regulations. The enclosed conveying system prevents dust from being released into the air, protecting both workers and the surrounding environment. Another key benefit is the reduction in material loss during transportation. Traditional methods often result in a certain percentage of material being lost due to spillage or leakage, but pneumatic conveying systems minimize this loss, ensuring that more of the valuable phosphate powder reaches its destination. Furthermore, the systems enhance operational efficiency by automating the powder handling process, reducing downtime and increasing production throughput. The precise control of flow rates and pressure allows for consistent product quality, which is crucial for maintaining customer satisfaction and market competitiveness. Finally, the energy-efficient design of the systems helps companies reduce operational costs, making the investment in pneumatic conveying systems a financially sound decision in the long run.
Customized Solutions for Diverse Phosphate Powder Handling Needs
HeadPowder understands that different clients have unique phosphate powder handling requirements. Therefore, the company provides customized pneumatic conveying solutions tailored to each client's specific needs. The design process begins with a thorough analysis of the client's production process, including the type and quantity of phosphate powder, the distance and layout of the conveying route, and the required output capacity. Based on this analysis, HeadPowder's engineering team designs a system that optimizes performance, efficiency, and cost. The company offers a range of system configurations, including dilute phase and dense phase conveying systems, to suit different application scenarios. For example, dilute phase systems are suitable for long-distance conveying with low material concentration, while dense phase systems are ideal for short-distance conveying with high material concentration and minimal pressure drop. Additionally, HeadPowder provides comprehensive after-sales services, including installation, commissioning, and maintenance, to ensure that the conveying systems operate at peak performance throughout their service life. The company's team of experienced engineers and technicians is available to provide technical support and troubleshooting services, ensuring that clients can maximize the benefits of their investment.
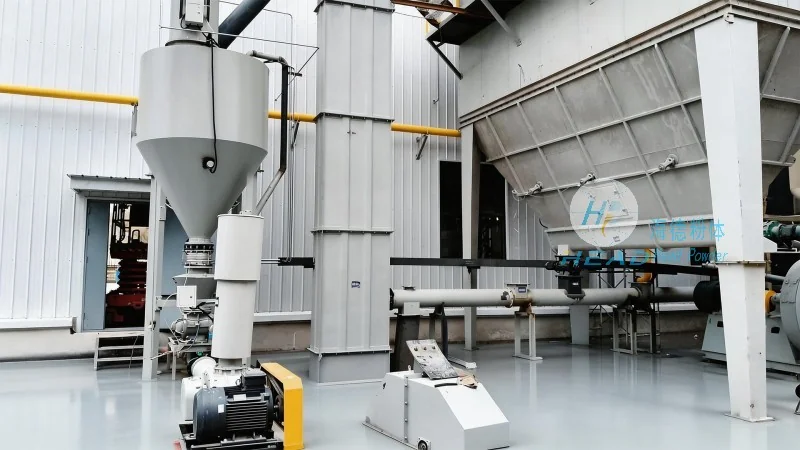
Conclusion and Contact Information
Phosphate powder pneumatic conveying solutions from Shandong HeadPowder Engineering Co., Ltd. represent a significant advancement in powder handling technology, offering efficient, reliable, and environmentally friendly solutions for the agricultural and chemical industries. By leveraging advanced engineering and technology, HeadPowder provides customized systems that meet the specific needs of clients, enhancing operational efficiency, reducing costs, and improving product quality. For companies looking to upgrade their phosphate powder handling systems, HeadPowder is a trusted partner that delivers high-quality, reliable solutions. Based in Shandong, China, HeadPowder serves clients worldwide, providing comprehensive support from design to installation and maintenance. Contact HeadPowder today to learn more about how their pneumatic conveying solutions can benefit your business.




