Efficient and reliable material handling is crucial in the agricultural and food processing industries, particularly when dealing with bulk commodities like rice grains. Pneumatic conveying systems offer a superior alternative to traditional methods such as belt conveyors or bucket elevators. These systems utilize air pressure to transport rice grains in a dust-free, hygienic manner, ensuring minimal product loss and contamination. This article explores the comprehensive solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying technology, tailored specifically for rice grain processing applications.
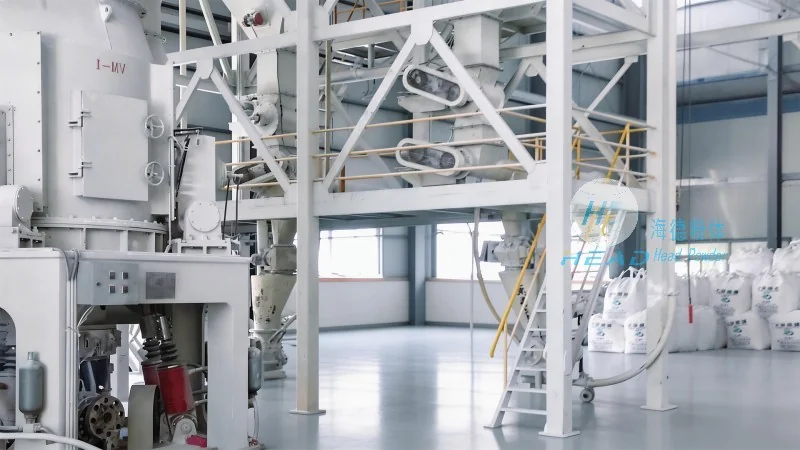
Key Features of Pneumatic Conveying for Rice Grain Handling
HeadPowder's rice grain pneumatic conveying solutions are designed to address the unique challenges of rice processing. The systems are equipped with high-efficiency airlocks and rotary valves that ensure smooth and continuous material flow. The use of stainless steel construction guarantees durability and compliance with food safety standards, making them suitable for both bulk storage and processing environments. Additionally, the systems are engineered to minimize product degradation, preserving the quality and nutritional value of the rice grains during transport. The advanced control systems allow for precise regulation of air pressure and flow rates, optimizing energy consumption while maintaining consistent performance.
Customized Solutions for Diverse Rice Processing Needs
Recognizing that rice processing facilities vary in scale and operational requirements, HeadPowder offers customized pneumatic conveying solutions. Whether for small-scale rice mills or large industrial processing plants, the company's engineers work closely with clients to design systems that meet specific throughput, space constraints, and budget considerations. The solutions can be integrated with existing infrastructure or serve as standalone systems, providing flexibility in installation and operation. The company's expertise in material flow analysis ensures that the designed systems achieve optimal performance, reducing downtime and maintenance costs over the long term.
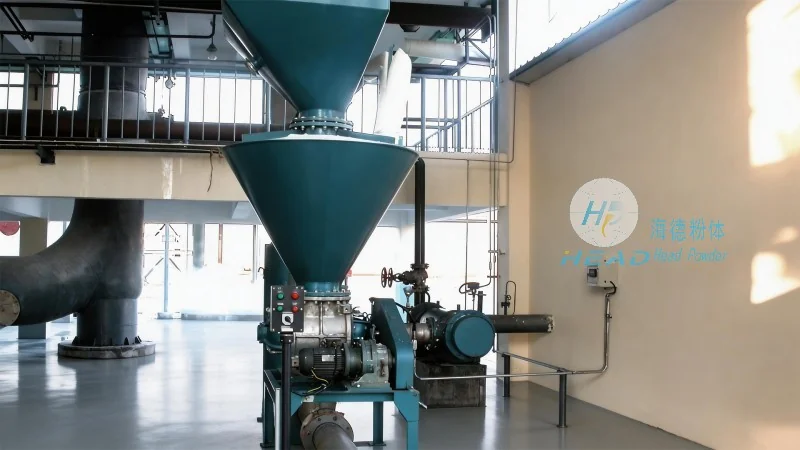
Benefits of Choosing HeadPowder's Pneumatic Conveying Systems
Implementing HeadPowder's rice grain pneumatic conveying solutions brings numerous advantages to rice processing operations. The primary benefit is the significant reduction in labor costs associated with manual handling and cleaning of traditional conveyor systems. The dust-free operation also enhances workplace safety and reduces the risk of respiratory issues among workers. Furthermore, the hygienic design of the systems helps maintain product purity, which is critical for meeting food safety regulations and consumer expectations. The energy-efficient design contributes to lower operational costs, making the investment in pneumatic conveying systems a cost-effective choice for long-term profitability.
Technical Specifications and Performance Metrics
HeadPowder's rice grain pneumatic conveying systems are built with robust components that ensure reliable performance under demanding conditions. The systems are available in various configurations, including positive pressure and negative pressure designs, to suit different application requirements. The positive pressure systems are ideal for long-distance transport and vertical lifting, while the negative pressure systems are suitable for handling fine particles and preventing product spillage. The performance of these systems is measured by key metrics such as conveying capacity, air consumption rate, and pressure drop. HeadPowder's solutions typically achieve conveying capacities ranging from 1 to 50 tons per hour, with air consumption rates optimized to minimize energy usage. The pressure drop across the system is carefully controlled to ensure efficient operation and reduce energy waste.
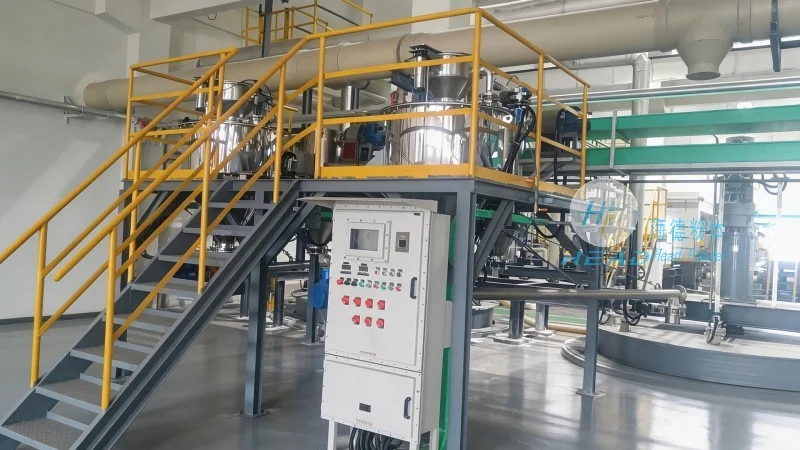
Installation and Maintenance Support
HeadPowder provides comprehensive support throughout the entire lifecycle of the pneumatic conveying system. From initial site assessment and system design to installation and commissioning, the company's team of experienced engineers ensures that the system is installed correctly and operates as intended. The maintenance services offered include regular inspections, component replacement, and troubleshooting to prevent unexpected downtime. The company's commitment to customer satisfaction is reflected in its after-sales support, which includes technical assistance and spare parts availability. By partnering with HeadPowder, rice processing facilities can rely on a reliable and efficient material handling solution that meets their operational needs and enhances overall productivity.
Conclusion
In conclusion, pneumatic conveying systems represent a modern and effective solution for rice grain handling in the agricultural and food processing industries. Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted provider of these systems, offering customized, high-quality solutions that address the specific requirements of rice processing operations. By leveraging advanced technology and expert engineering, HeadPowder's solutions contribute to improved efficiency, reduced costs, and enhanced product quality in rice grain handling processes. For businesses seeking to optimize their material handling operations, HeadPowder's pneumatic conveying systems provide a reliable and sustainable choice.




