Efficient and reliable material handling is a critical requirement in various industrial applications, particularly when dealing with fine sand and gravel. Traditional methods such as belt conveyors or bucket elevators often face challenges like material degradation, blockages, and high maintenance costs. Pneumatic conveying systems offer a superior alternative, providing a clean, dust-free, and energy-efficient way to transport these materials over long distances. This article explores the design, functionality, and benefits of a specialized pneumatic conveying system tailored for fine sand and gravel, presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
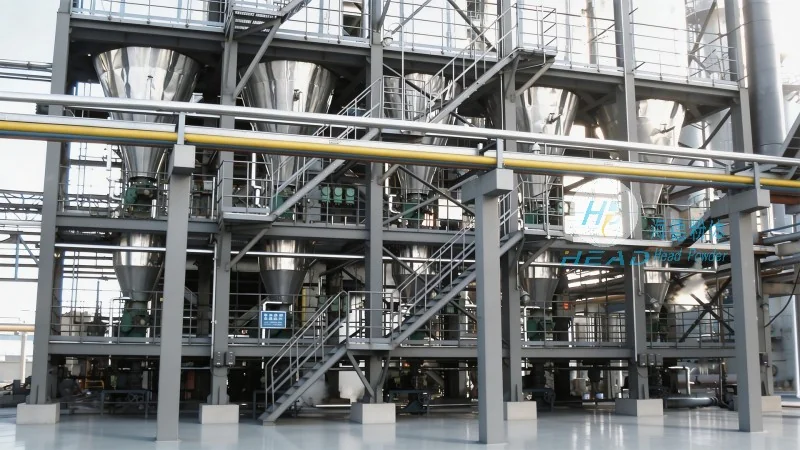
Understanding Pneumatic Conveying Technology
Pneumatic conveying systems utilize air pressure to transport bulk materials through a pipeline. In the case of fine sand and gravel, these systems are engineered to handle materials with specific particle sizes and moisture content. The technology involves two primary modes: dilute phase and dense phase. Dilute phase systems use high-velocity air to move materials in a suspended state, suitable for short to medium distances. Dense phase systems, on the other hand, use lower air velocities and higher material concentrations, ideal for longer distances and more delicate materials. The choice between these modes depends on the application requirements, including material characteristics, distance, and desired flow rate.
Key Components of the System
The pneumatic conveying system for fine sand and gravel consists of several essential components that work in harmony to ensure smooth operation. These include a material feeder, which accurately controls the flow rate of the sand or gravel into the system; a conveying line, typically made of corrosion-resistant materials like stainless steel or PVC to prevent material buildup and wear; a blower or compressor that generates the necessary air pressure; and a receiver or discharge unit where the material is collected. Additionally, the system may incorporate features such as air filters to maintain air quality, pressure regulators to control system pressure, and monitoring devices to track performance and detect any issues in real-time.
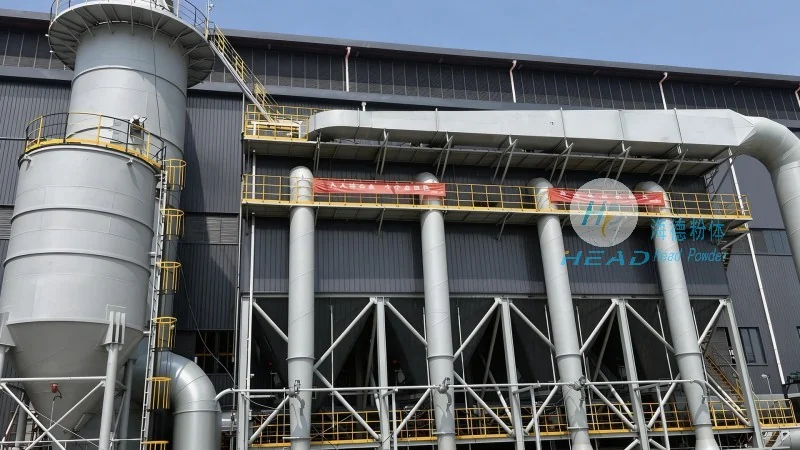
Benefits of Using a Pneumatic Conveying System
Implementing a pneumatic conveying system for fine sand and gravel offers numerous advantages over traditional methods. Firstly, it provides a dust-free and clean operation, which is crucial in environments where dust can affect product quality or pose health hazards. Secondly, the system minimizes material degradation, as the materials are transported without direct contact with other surfaces, reducing breakage and loss of fines. Thirdly, it reduces maintenance costs and downtime, as the system has fewer moving parts compared to mechanical conveyors, and the risk of blockages is significantly lower. Fourthly, it allows for flexible and scalable solutions, as the system can be easily expanded or reconfigured to accommodate changing production needs. Lastly, it enhances safety by eliminating the need for manual handling of bulk materials, reducing the risk of accidents and injuries.
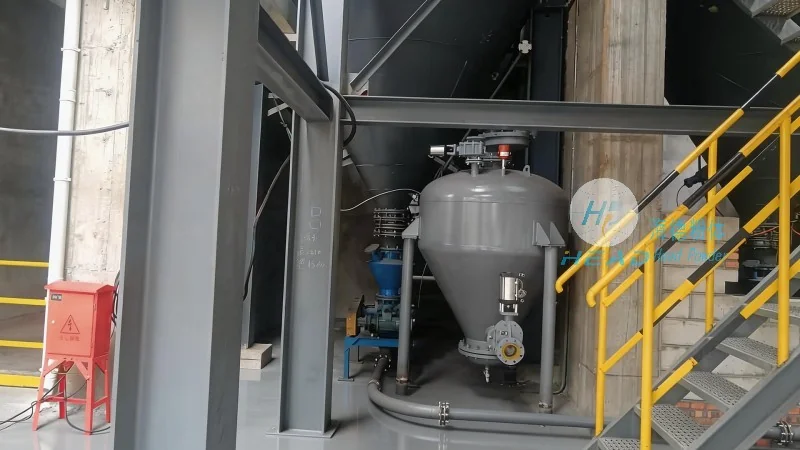
Application Scenarios
The pneumatic conveying system is widely used in various industries that handle fine sand and gravel, including construction, mining, and manufacturing. In the construction industry, it is commonly used to transport sand and gravel from storage silos to mixing plants or concrete production lines. In mining operations, it helps in transporting ore or crushed rock from processing facilities to storage areas. In manufacturing, it is used in processes such as cement production, where fine sand is used as an aggregate. The system's ability to handle materials with different particle sizes and moisture content makes it versatile for a wide range of applications.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a reputable company specializing in the design, manufacturing, and installation of pneumatic conveying systems. With years of experience in the industry, the company has developed a deep understanding of material handling challenges and has developed innovative solutions to address them. The company's team of engineers and technicians is dedicated to providing customized solutions that meet the specific needs of each client, ensuring optimal performance and efficiency. HeadPowder's commitment to quality and customer satisfaction has earned it a strong reputation in the market, making it a trusted partner for businesses seeking reliable material handling solutions.




