HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and application of negative pressure vacuum powder conveying systems. These systems are engineered to efficiently transport dry powders and bulk materials over long distances with precision and reliability. This article delves into the fundamental principles behind such systems and highlights the key working scene characteristics that make them indispensable in various industrial applications.
Understanding the Core Principle of Negative Pressure Vacuum Conveying
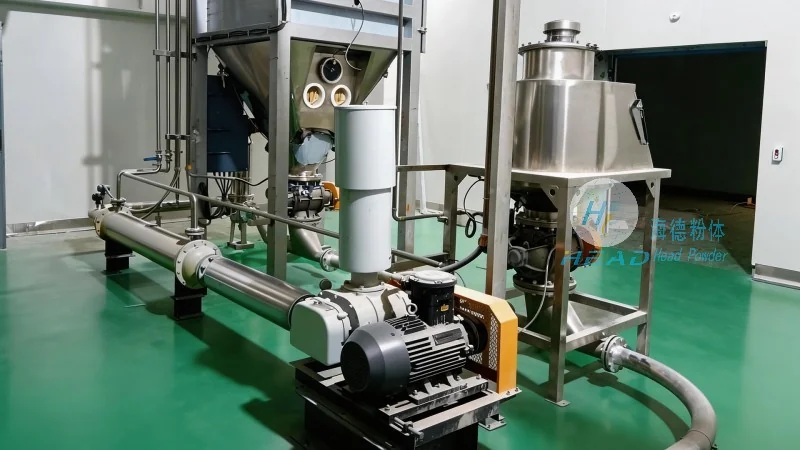
The negative pressure vacuum powder conveying system operates on the principle of creating a partial vacuum within the conveying line. By drawing air and the material particles into the system, the equipment uses a combination of air flow and pressure differentials to move powders from the source to the destination. The process involves several critical components, including a vacuum pump, a filter system, and a series of pipes or hoses that form the conveying path. The vacuum pump generates the necessary suction force, while the filter ensures that the air released back into the environment is clean and free from dust particles. This method is particularly effective for handling fine powders and granular materials that are prone to dusting or clogging in traditional pneumatic conveying systems.
Key Working Scene Characteristics and Applications
The negative pressure vacuum conveying system is characterized by several distinct advantages that make it suitable for a wide range of industrial scenarios. Firstly, it operates under low pressure, which reduces the risk of material degradation and equipment wear compared to positive pressure systems. This makes it ideal for transporting heat-sensitive or fragile powders without compromising their quality. Secondly, the system is highly flexible in terms of layout and can be adapted to complex or irregular plant layouts, as the conveying lines can be easily reconfigured or extended. This flexibility is crucial for facilities that require frequent changes in production processes or material handling routes.
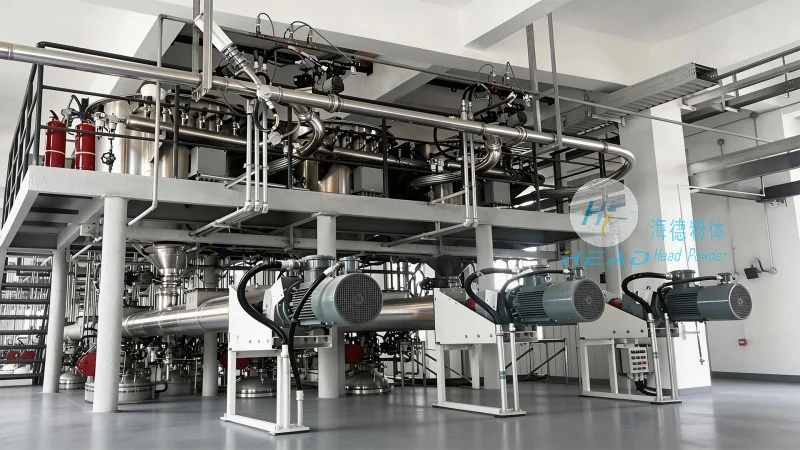
Another significant characteristic is the system's ability to handle powders with varying particle sizes and moisture content. The negative pressure approach allows for the efficient transport of both fine powders and larger granules, making it versatile for applications in pharmaceuticals, food processing, chemical manufacturing, and mining industries. The system's self-cleaning capabilities, facilitated by the filter and the way air is drawn through the material, also contribute to its reliability and low maintenance requirements. This is particularly beneficial for continuous production lines where downtime can lead to significant operational costs.
Company Background and Expertise
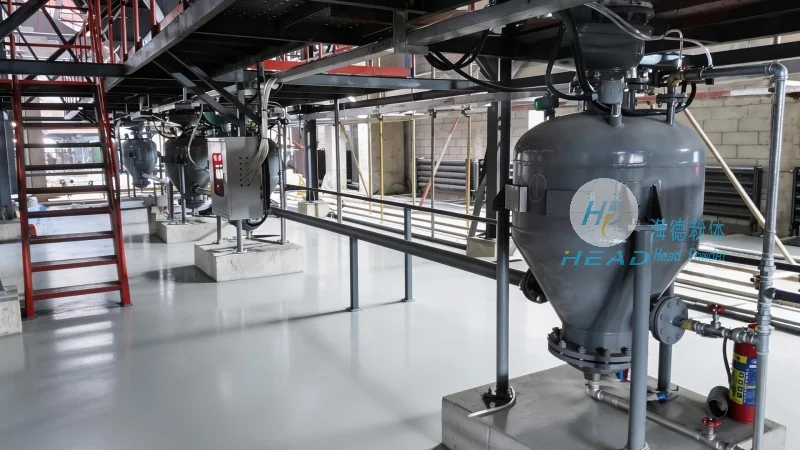
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has established itself as a trusted name in the powder handling industry. With years of experience and a commitment to innovation, the company has developed advanced negative pressure vacuum conveying systems that meet the stringent requirements of modern industrial applications. The company's team of engineers and technicians work closely with clients to understand their specific material handling challenges and design customized solutions that optimize efficiency and safety. By leveraging cutting-edge technology and rigorous quality control measures, HeadPowder ensures that its systems deliver consistent performance and long-term reliability.
Conclusion and Industry Impact
In conclusion, the negative pressure vacuum powder conveying system represents a sophisticated and efficient solution for the transportation of dry powders and bulk materials. Its ability to operate under low pressure, handle diverse materials, and adapt to complex layouts makes it a preferred choice for industries seeking reliable and cost-effective material handling solutions. As a leading provider in this field, HeadPowder Engineering Co., Ltd. continues to advance the technology and provide tailored solutions that address the evolving needs of industrial operations worldwide.




