Understanding the fundamental principles and practical operational scenarios of brown sugar powder conveying systems is crucial for optimizing material handling processes in various industrial applications. These systems are designed to efficiently transport bulk brown sugar powder from storage to processing or packaging stages, ensuring minimal loss, consistent flow, and adherence to quality standards. The core components and operational mechanisms of such systems play a pivotal role in enhancing productivity and maintaining product integrity throughout the supply chain.
Core Principles of Brown Sugar Powder Conveying Systems
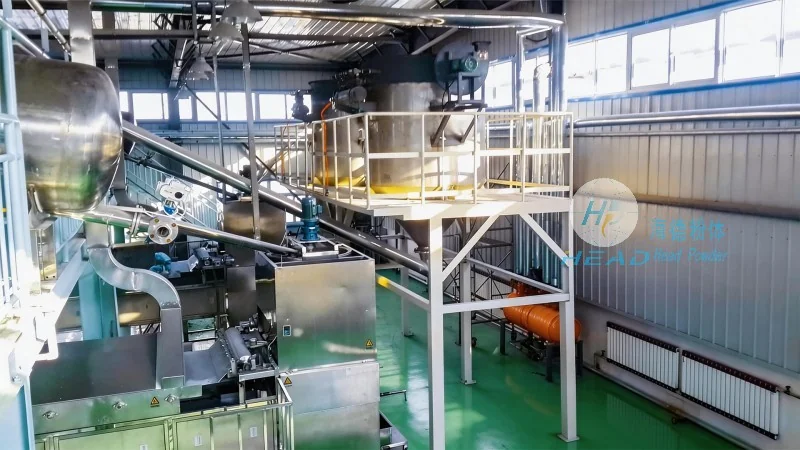
The operation of brown sugar powder conveying systems is grounded in several key principles that ensure reliable and efficient material transport. Firstly, the system relies on the principles of fluidization and pneumatic or mechanical movement to move the powder. Fluidization involves creating a gas-solid two-phase flow by introducing air or other gases through the powder bed, which reduces the powder's apparent density and allows for smooth transport. This method is particularly effective for fine powders like brown sugar, as it minimizes particle agglomeration and ensures uniform flow. Secondly, the system employs precise control mechanisms to regulate the flow rate, pressure, and velocity of the conveying medium. These controls are essential for maintaining consistent material throughput and preventing issues such as blockages or overloading of the conveying lines. Additionally, the design incorporates features that address the hygroscopic nature of brown sugar, such as moisture-resistant materials and sealed conveying paths, to prevent caking or clumping during transport.
Operational Scenarios and Applications
Brown sugar powder conveying systems are widely utilized across diverse industrial settings, each with specific requirements tailored to the production environment. In sugar refineries, these systems are integral to the downstream processing of raw sugar, where they transport refined brown sugar from storage silos to packaging lines. The systems are designed to handle large volumes of powder, often operating continuously to meet high production demands. In food processing facilities, the conveying systems are used to move brown sugar from bulk storage to mixing or blending units, ensuring that the powder is delivered in a controlled manner to maintain the consistency of final products. Furthermore, in pharmaceutical and nutraceutical industries, where brown sugar may be used as an ingredient, the conveying systems must adhere to stringent hygiene and contamination control standards. This includes the use of stainless steel components, sealed conveyor lines, and advanced filtration systems to prevent cross-contamination and maintain product purity. The versatility of brown sugar powder conveying systems also extends to smaller-scale operations, such as in bakeries or confectionery shops, where they facilitate the efficient transfer of brown sugar from bulk containers to production lines, improving workflow efficiency and reducing manual handling efforts.
Key Components and Technical Specifications
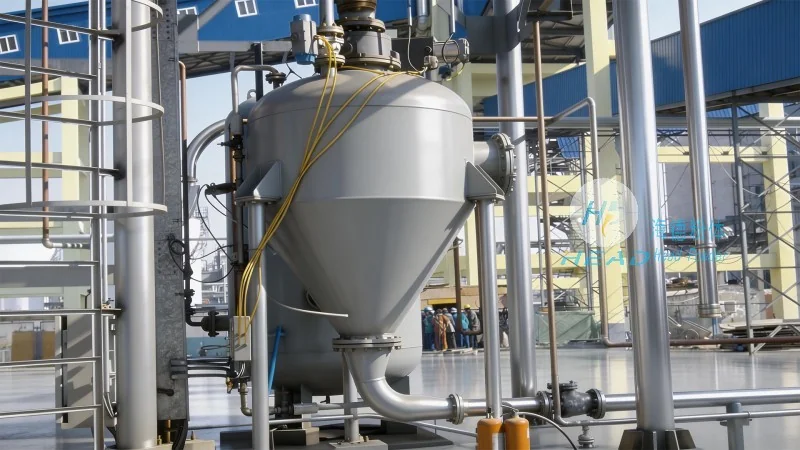
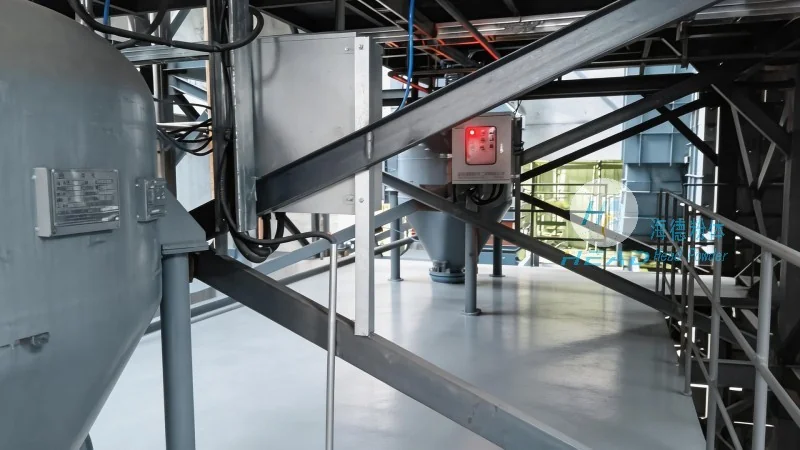
HeadPowder, a leading provider of industrial conveying solutions, offers advanced brown sugar powder conveying systems that incorporate cutting-edge technology and robust design. The systems typically consist of several key components, including a hopper for material storage, a conveyor line (either pneumatic or mechanical), a control panel for operational management, and a discharge mechanism for material release. The hopper is designed with a conical or rectangular shape to facilitate uniform material flow and prevent bridging or arching, which are common issues in powder handling. The conveyor line may be pneumatic, utilizing air pressure to move the powder through a pipeline, or mechanical, employing screws, belts, or buckets to transport the material. The choice between pneumatic and mechanical systems depends on factors such as the powder's characteristics, required throughput, and space constraints. For brown sugar, which is a fine, hygroscopic powder, pneumatic conveying is often preferred due to its ability to handle low to medium pressure systems while minimizing product degradation. The control panel integrates sensors and controllers that monitor parameters such as pressure, flow rate, and temperature, providing real-time feedback and allowing for automated adjustments to maintain optimal performance. Additionally, the discharge mechanism is designed to ensure smooth release of the powder into the next processing stage, preventing spillage or blockage.
Advantages and Benefits of HeadPowder's Conveying Systems
Implementing a brown sugar powder conveying system from HeadPowder Engineering Co., Ltd. offers numerous advantages for industrial operations. The primary benefit is enhanced efficiency, as these systems can handle large volumes of brown sugar powder with minimal manual intervention, reducing labor costs and increasing production throughput. The systems also contribute to improved product quality by maintaining consistent flow and preventing contamination or degradation during transport. This is particularly important for brown sugar, which is sensitive to moisture and temperature changes. Additionally, the systems are designed for durability and low maintenance, utilizing high-quality materials such as stainless steel and corrosion-resistant components to withstand the harsh conditions of industrial environments. The modular design of the systems allows for easy integration into existing production lines, minimizing downtime during installation and ensuring a smooth transition to automated material handling. Furthermore, the systems are equipped with advanced safety features, including pressure relief valves and emergency stop mechanisms, to protect operators and equipment from potential hazards. The energy efficiency of these systems is another key advantage, as they are designed to operate with minimal power consumption while maintaining high performance, reducing operational costs and environmental impact.
Conclusion and Company Overview
In conclusion, brown sugar powder conveying systems are essential components in modern industrial operations, providing reliable and efficient material transport while maintaining product quality and operational efficiency. HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced conveying solutions tailored to the unique needs of brown sugar processing. With a focus on innovation, quality, and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry, delivering systems that meet the highest standards of performance and reliability. By leveraging the core principles of fluidization and precise control, their conveying systems ensure smooth, consistent transport of brown sugar powder across various operational scenarios, from large-scale refineries to smaller-scale food processing facilities. The company's commitment to excellence and continuous improvement ensures that their products remain at the forefront of industrial material handling technology, supporting the growth and success of their clients in the competitive brown sugar market.




