

How to Choose the Right Pneumatic Conveying System for Your Heptahydrate Magnesium Sulfate Handling Process?
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of specialized engineering solutions tailored for the handling and processing of industrial materials. With a focus on precision and efficiency, our company has built a reputation for delivering high-quality pneumatic conveying systems that meet the unique demands of processes involving heptahydrate magnesium sulfate. Based in Shandong, China, HeadPowder combines technical expertise with practical experience to offer customized solutions that enhance operational performance and reliability.
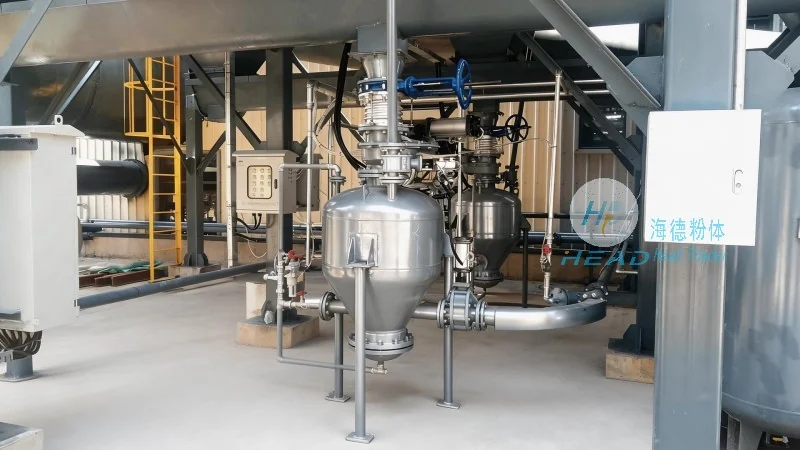
Pneumatic Conveying Systems for Heptahydrate Magnesium Sulfate Handling
When managing heptahydrate magnesium sulfate, selecting the right pneumatic conveying system is crucial for maintaining product integrity, ensuring safe and efficient material transport, and optimizing overall process flow. Our systems are designed to handle the specific characteristics of this chemical, including its granular or powder form, moisture content, and potential dust generation. By leveraging advanced technology and engineering principles, we develop solutions that minimize product degradation, reduce downtime, and improve cost-effectiveness in material handling operations.
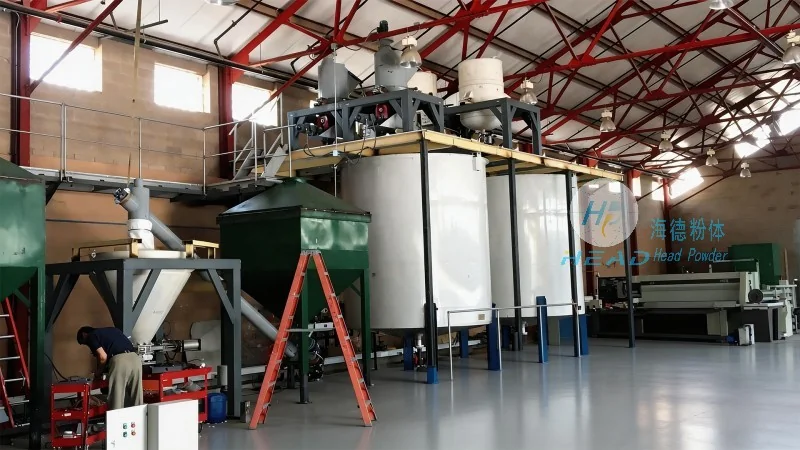
Key Considerations for Selecting a Pneumatic Conveying System
Choosing the appropriate pneumatic conveying system for heptahydrate magnesium sulfate handling requires careful evaluation of several critical factors. First, the system must be capable of handling the material's physical properties, such as particle size, density, and flowability. Second, the design should address the need for maintaining product purity and preventing contamination, which is essential in applications where the material is used in pharmaceutical, food, or chemical industries. Third, energy efficiency and operational costs are significant considerations, as these systems often run continuously in industrial settings. Additionally, the system's scalability and adaptability to future process changes are important for long-term investment value. HeadPowder’s team of engineers conducts thorough assessments of these factors to recommend systems that align with the client's specific operational requirements and budget constraints.
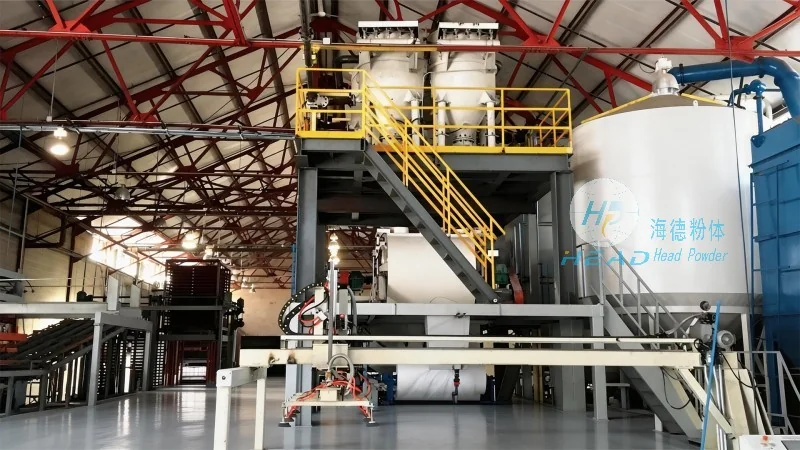
Advantages of Our Pneumatic Conveying Solutions
Our pneumatic conveying systems for heptahydrate magnesium sulfate offer several key advantages that set them apart from conventional material handling methods. One primary benefit is the ability to transport materials in a closed system, which significantly reduces dust exposure and improves workplace safety. This is particularly important for heptahydrate magnesium sulfate, as it can generate fine particles that pose health risks if not properly contained. Another advantage is the system's flexibility in handling varying material flow rates and distances, allowing for seamless integration into existing production lines or new facility setups. The systems also provide better control over material distribution, ensuring consistent feed rates to downstream processes like mixing, packaging, or further processing. Furthermore, our solutions are engineered for durability and low maintenance, reducing operational disruptions and extending the lifespan of the equipment. By incorporating these features, our systems contribute to improved overall productivity and reduced environmental impact in material handling operations.
Real-World Applications and Success Stories
HeadPowder has successfully implemented pneumatic conveying systems for heptahydrate magnesium sulfate in various industrial settings. For example, in a pharmaceutical manufacturing facility, our system was integrated to transport the material from storage silos to a mixing unit, ensuring a dust-free and controlled environment that meets stringent regulatory standards. The system's ability to handle fine particles without clogging or degradation was critical in maintaining product quality and compliance. In another case, a chemical processing plant adopted our solution to improve the efficiency of material transfer between different processing stages, resulting in a 20% reduction in handling time and a corresponding decrease in labor costs. These success stories highlight the effectiveness of our systems in addressing the unique challenges of handling heptahydrate magnesium sulfate, demonstrating our commitment to delivering solutions that meet both technical and operational needs.
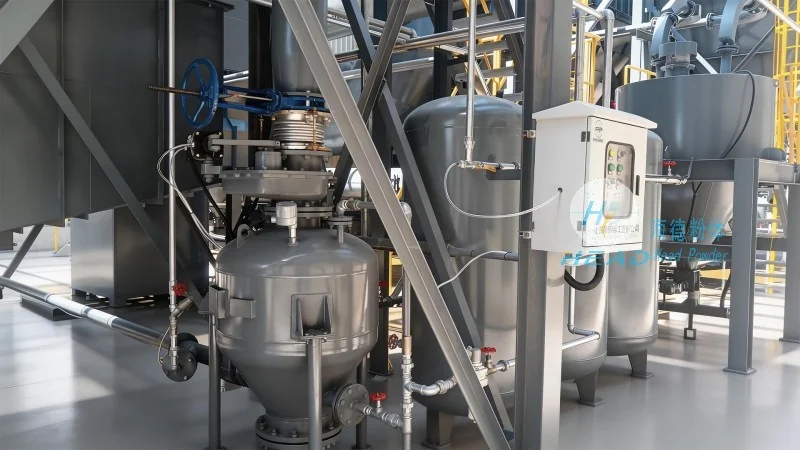
Conclusion: Partnering with HeadPowder for Reliable Pneumatic Conveying Solutions
When selecting a pneumatic conveying system for your heptahydrate magnesium sulfate handling process, it is essential to choose a partner with deep expertise and a proven track record in industrial material handling. Shandong HeadPowder Engineering Co., Ltd. stands out as a trusted provider that combines technical innovation with practical application knowledge. Our systems are designed to address the specific requirements of heptahydrate magnesium sulfate, ensuring safe, efficient, and cost-effective material transport. By working closely with our engineering team, clients can benefit from customized solutions that enhance operational performance, improve product quality, and contribute to long-term business success. Whether you are upgrading an existing system or planning a new facility, HeadPowder is ready to provide the expertise and support needed to achieve your material handling goals.