Feather powder pneumatic conveying equipment is a specialized system designed for the efficient transport of fine powder materials, such as feather powder, in industrial applications. Understanding its working principle and key features is crucial for selecting the right equipment for specific operational needs. This article explores the fundamental mechanisms behind these machines and highlights their distinctive attributes that make them suitable for handling delicate and high-value powder products.
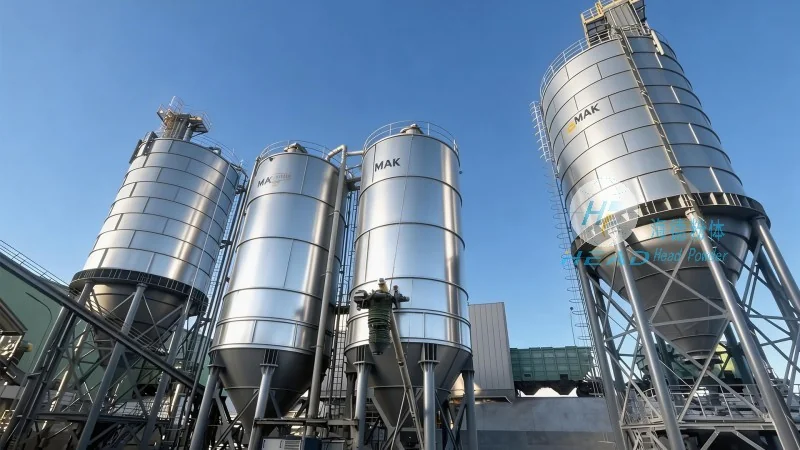
Working Principle of Feather Powder Pneumatic Conveying Equipment
The core working principle of a feather powder pneumatic conveying system revolves around the use of air pressure to move powder particles through a pipeline. The process typically involves several key components and steps. First, the powder is fed into a hopper or feeder, where it is then introduced into a pipeline. Simultaneously, a fan or blower generates a flow of air within the pipeline, creating a pressure differential that propels the powder particles forward. The air acts as a carrier, suspending the powder and transporting it from the source to the destination. The system may employ different modes of operation, including positive pressure (where air is forced into the system) or negative pressure (where air is drawn out), depending on the specific design and application requirements. The efficiency of the conveying process is influenced by factors such as air velocity, particle size, and the density of the powder. Proper design ensures that the powder remains suspended in the air stream, preventing blockages and ensuring smooth transport. The equipment may also include features like cyclone separators or filters to separate the powder from the air at the receiving end, allowing for clean and efficient material handling.
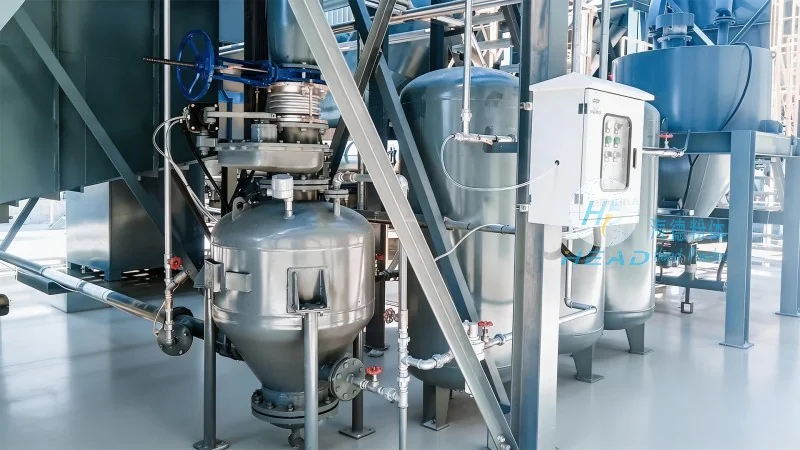
Key Features of Feather Powder Pneumatic Conveying Equipment
Feather powder pneumatic conveying equipment is characterized by several notable features that enhance its performance and suitability for handling delicate powder materials. One of the primary features is its ability to handle fine and abrasive powders without causing excessive wear or damage to the system components. The design incorporates materials resistant to corrosion and abrasion, ensuring long-term durability. Another key feature is the system's flexibility in terms of layout and configuration. It can be adapted to various industrial settings, with the ability to transport materials over long distances or through complex piping networks. The equipment also offers high efficiency in terms of material transport, minimizing losses and ensuring consistent flow rates. Additionally, the system is designed to be low maintenance, with components that are easy to access and replace, reducing downtime and operational costs. The use of air as the conveying medium also provides a hygienic and clean environment, which is particularly important for food-grade or pharmaceutical applications where contamination must be avoided. The equipment may also include monitoring and control systems to optimize performance and ensure safe operation. These features collectively make feather powder pneumatic conveying equipment an ideal solution for industries requiring reliable and efficient transport of fine powder materials.
Applications and Benefits in Industrial Settings
Feather powder pneumatic conveying equipment finds wide applications across various industrial sectors, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, it is used for transporting feather meal or other fine powders used in animal feed or human food products. The system ensures that the powder is handled hygienically and without contamination, meeting stringent food safety standards. In pharmaceutical applications, the equipment is employed to transport active ingredients or other fine powders used in drug formulation, where precision and cleanliness are paramount. The benefits of using this equipment extend beyond just efficient transport; it also contributes to improved product quality by minimizing dust and particle loss. The system's ability to maintain consistent flow rates and pressure levels ensures that the powder is delivered to the processing line in a controlled manner, reducing variability in downstream operations. Furthermore, the low energy consumption of pneumatic conveying systems compared to traditional methods like belt conveyors makes them cost-effective in the long run. The equipment also offers scalability, allowing it to be expanded or modified as production needs change. Overall, the use of feather powder pneumatic conveying equipment enhances operational efficiency, reduces labor costs, and improves product quality in industrial settings.
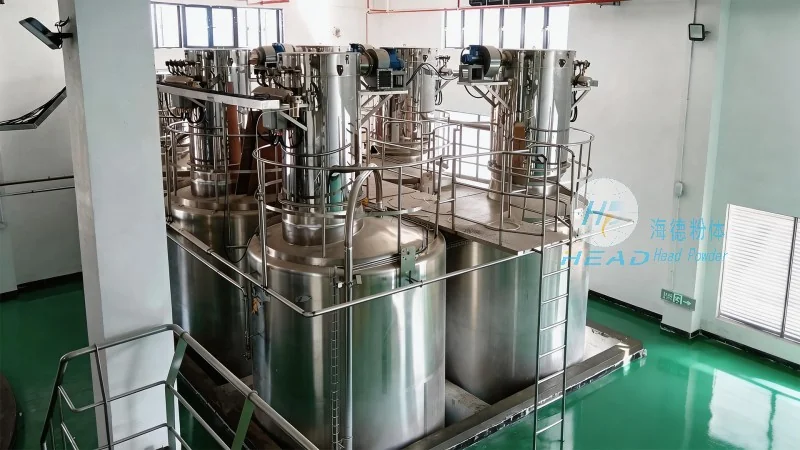
Conclusion and Company Overview
Feather powder pneumatic conveying equipment is a sophisticated and efficient solution for transporting fine powder materials, offering a range of benefits that address the challenges of traditional material handling methods. The working principle, which relies on air pressure to move powder particles, combined with key features such as durability, flexibility, and hygiene, makes it a preferred choice for industries dealing with delicate and high-value powders. The equipment is designed to handle the specific requirements of feather powder, ensuring minimal damage and maximum efficiency. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing customized solutions tailored to the unique needs of each client. With a focus on quality and innovation, the company ensures that its products meet the highest standards of performance and reliability. Based in Shandong, China, HeadPowder has established itself as a trusted partner in the industrial equipment sector, delivering solutions that enhance productivity and operational excellence. Whether for food processing, pharmaceuticals, or other industries, the feather powder pneumatic conveying equipment from HeadPowder offers a reliable and efficient means of material transport, contributing to the overall success of industrial operations.




