Understanding the working principle and features of coal ash material handling is crucial for optimizing industrial processes in waste management and energy sectors. This article provides a detailed overview of the mechanisms and characteristics of coal ash material handling systems, presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions in China.
Working Principle of Coal Ash Material Handling Systems
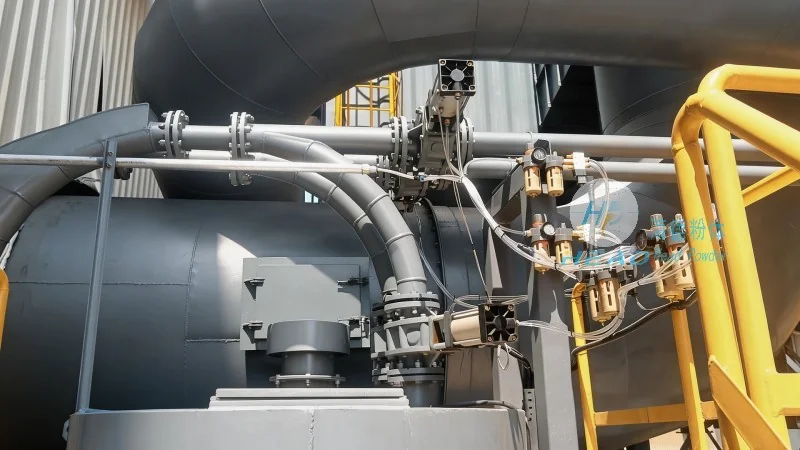
Coal ash material handling systems operate on principles that ensure efficient transport, storage, and processing of coal ash, a byproduct of coal combustion. The core components and operational mechanisms include:
1. **Conveying Equipment**: Systems typically utilize various types of conveyors such as belt conveyors, screw conveyors, and pneumatic conveyors. Belt conveyors are widely used for horizontal and inclined transport due to their high load capacity and low maintenance requirements. Screw conveyors are effective for vertical or inclined transport, especially in confined spaces. Pneumatic conveyors, or airslides, use air pressure to move fine coal ash particles, offering flexibility in layout and minimal mechanical parts.
2. **Feeding and Dosing Mechanisms**: Proper feeding and dosing are critical to maintain consistent material flow. Feeder devices, including rotary valves and star feeders, regulate the amount of coal ash entering the conveying system. These mechanisms ensure uniform material distribution and prevent blockages or overloading of the conveyor.
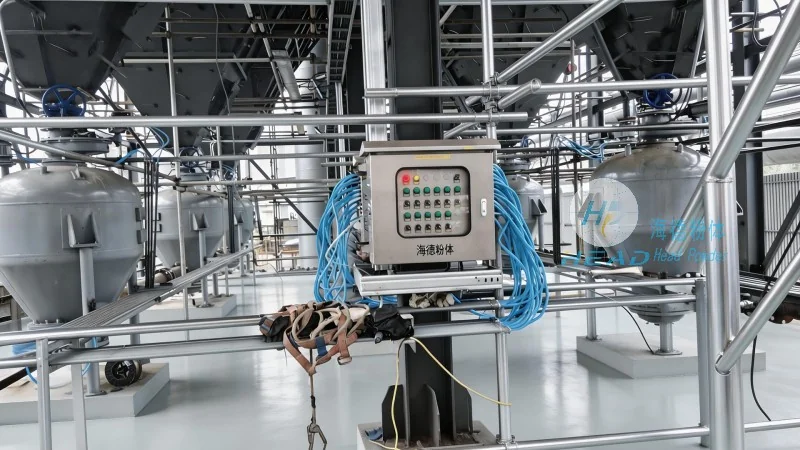
3. **Control Systems**: Modern coal ash material handling systems are equipped with advanced control systems that monitor and adjust operational parameters in real-time. Sensors for level, flow, and temperature, along with programmable logic controllers (PLCs), enable automated operation and enhance safety by detecting anomalies and triggering emergency stops when necessary.
Key Features of Coal Ash Material Handling Systems
Coal ash material handling systems exhibit several notable features that contribute to their effectiveness and adaptability in industrial applications:
1. **High Efficiency and Capacity**: These systems are designed to handle large volumes of coal ash with minimal downtime. The robust construction and efficient conveying mechanisms ensure consistent throughput, meeting the demands of power plants and waste processing facilities.
2. **Durability and Corrosion Resistance**: Coal ash is often abrasive and may contain acidic components, requiring equipment made from corrosion-resistant materials such as stainless steel or special alloys. This ensures long service life and reduces maintenance costs.
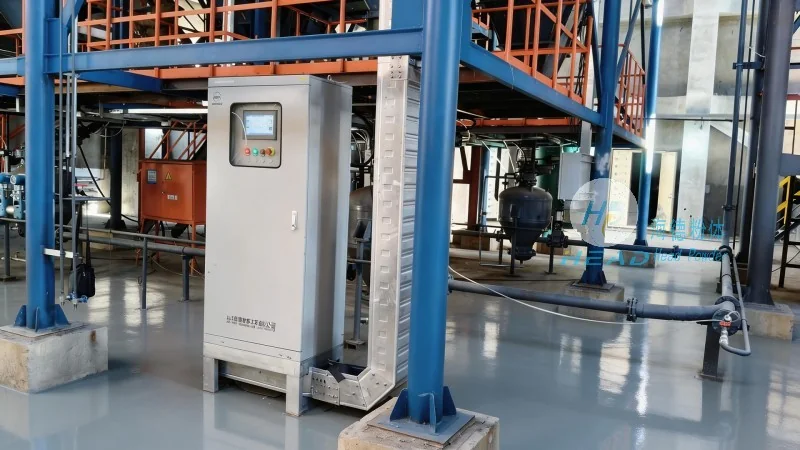
3. **Environmental Compliance**: Modern systems incorporate features to minimize dust emissions and noise pollution. Enclosed conveyor designs and dust collection systems help maintain environmental standards, making them suitable for operations in urban or sensitive areas.
4. **Modular and Scalable Design**: Coal ash material handling systems are often modular, allowing for easy expansion or integration with existing infrastructure. This flexibility enables companies to adapt their systems as production needs change, optimizing investment and operational efficiency.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a professional engineering company based in Shandong, China, specializing in the design, manufacturing, and installation of coal ash material handling systems. With years of experience in the industry, the company provides tailored solutions to meet the specific needs of clients in power generation, waste management, and related sectors. The company’s commitment to quality, innovation, and customer satisfaction has established it as a trusted partner in the field of industrial material handling.




