HeadPowder, a leading provider of bulk material handling solutions, specializes in the design and implementation of efficient silo material conveying systems. This article explores the fundamental working principles and key characteristics of such systems, offering insights into how they operate and their advantages in industrial applications.
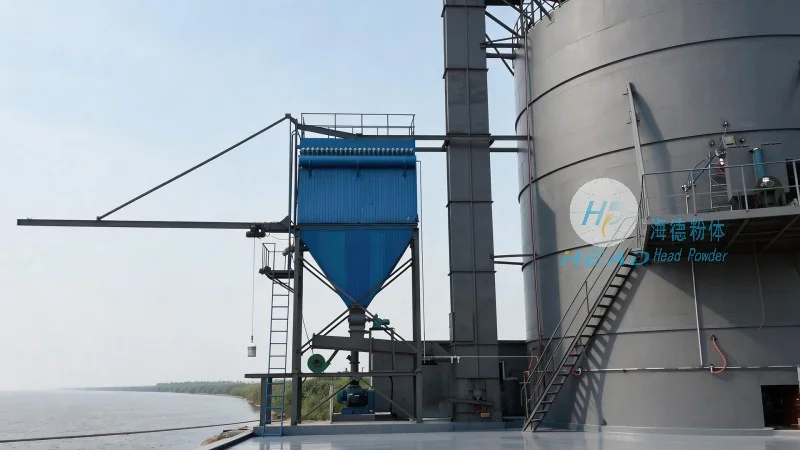
Company Profile and Background
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer and supplier based in Shandong, China. With years of experience in the field of bulk material handling, the company focuses on delivering high-quality equipment and services tailored to meet the diverse needs of clients across various industries. HeadPowder's expertise lies in the integration of advanced technologies and robust engineering to ensure reliable and efficient material transport within silo systems.
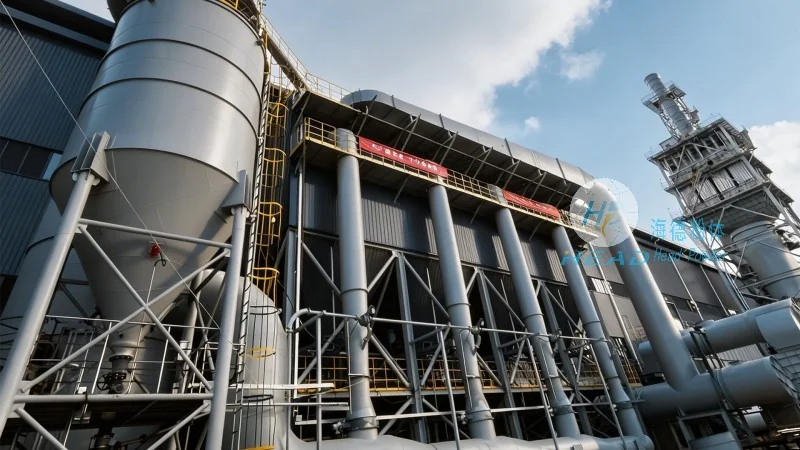
The Working Principle of Silo Material Conveying
The core function of a silo material conveying system is to transfer bulk materials from storage silos to processing or packaging equipment. The process typically involves several key components and operational steps. First, the material is stored in the silo, where it is held under controlled conditions to maintain quality and prevent degradation. When the material needs to be transported, a conveying device, such as a screw conveyor, pneumatic conveyor, or bucket elevator, is activated to draw the material from the silo's discharge point. The conveying mechanism then moves the material through a pipeline or conveyor structure to the target destination. This process ensures a continuous and controlled flow of material, minimizing downtime and maximizing operational efficiency.
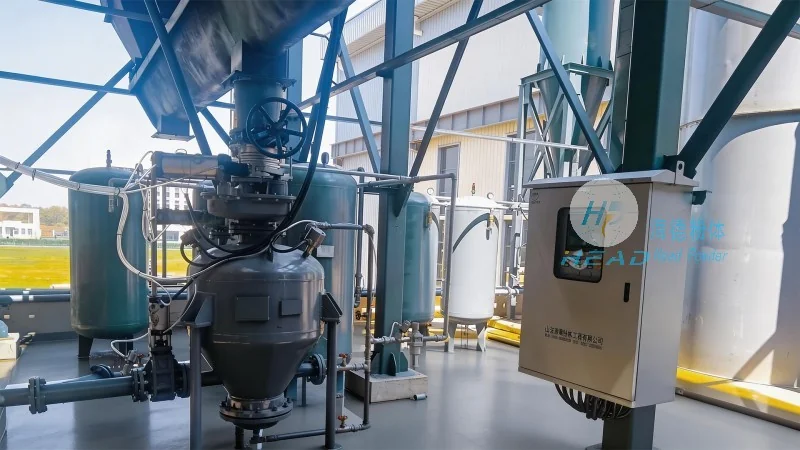
Key Features and Advantages of Silo Material Conveying Systems
Efficient silo material conveying systems are characterized by several important features that enhance their performance and reliability. One of the primary advantages is the ability to handle a wide range of bulk materials, including powders, granules, and bulk solids, with minimal maintenance. The systems are designed to operate under various environmental conditions, ensuring consistent performance even in challenging industrial settings. Another key feature is the integration of automation and control systems, which allow for precise regulation of material flow rates and pressure, reducing the risk of overfilling or underfilling. Additionally, these systems are built with durability and longevity in mind, using high-quality materials and robust construction to withstand heavy usage and harsh conditions. The result is a reliable and efficient solution for material handling that minimizes operational costs and maximizes productivity.
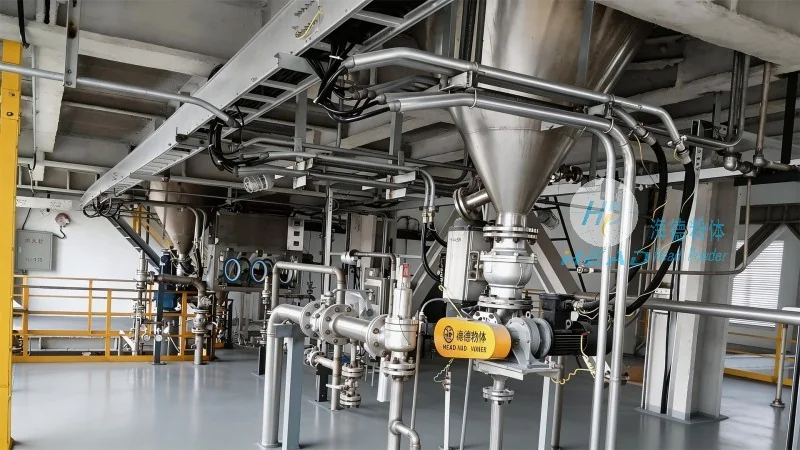
Conclusion
In summary, the working principle of silo material conveying systems involves the coordinated operation of storage, conveying, and control components to ensure the smooth transfer of bulk materials. The features of these systems, such as versatility, reliability, and automation, make them essential in modern industrial applications. HeadPowder, with its expertise and commitment to quality, continues to provide advanced solutions that meet the evolving needs of the bulk material handling industry.




