Working Principle and Features of Tonne Bag Unloading Powder Conveyors
Release time:2026-09-17 14:01:20
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer of powder handling equipment based in Shandong, China. The company specializes in developing and producing advanced tonne bag unloading powder conveyors, which are essential for efficient material transfer in various industrial applications.
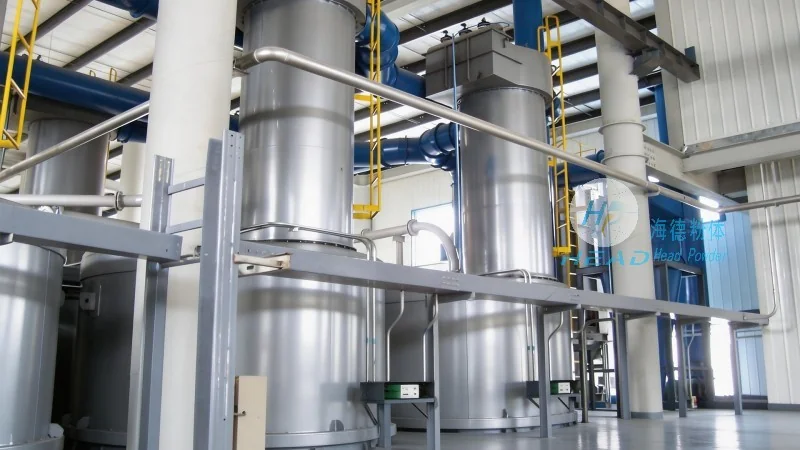
Working Principle of Tonne Bag Unloading Powder Conveyors
The tonne bag unloading powder conveyor is designed to automate the process of extracting bulk powders from large bags, typically with a capacity of one ton or more. The system operates by first positioning the tonne bag onto a designated loading platform. Once the bag is secured, an internal mechanism, such as a rotary valve or a screw conveyor, initiates the unloading process. This mechanism gradually discharges the powder from the bag into a hopper or a direct feeding system. Simultaneously, the conveyor may incorporate a pneumatic or mechanical transport system to move the discharged powder to the next processing stage. The entire operation is often controlled by an automated system, which ensures precise and consistent material flow, reducing the need for manual intervention and minimizing the risk of dust exposure.
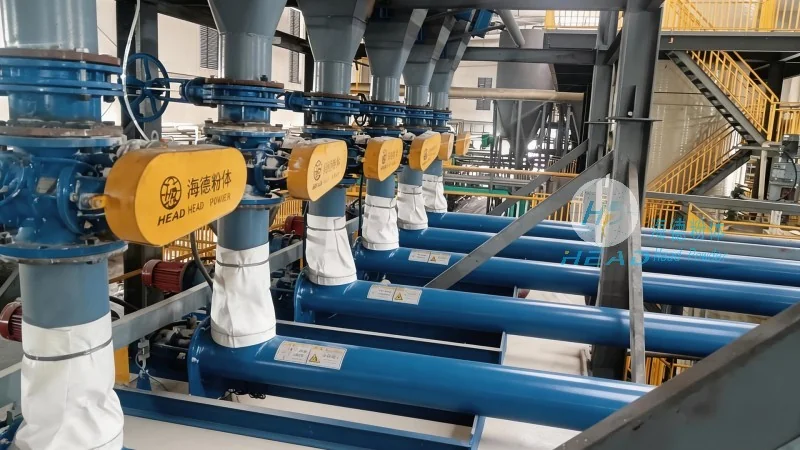
Key Features of Tonne Bag Unloading Powder Conveyors
HeadPowder's tonne bag unloading powder conveyors are engineered with several distinctive features that enhance their performance and reliability. One of the primary features is the enclosed design, which effectively contains dust and prevents environmental contamination, making them suitable for applications in industries where dust control is critical, such as pharmaceuticals and food processing. The conveyors are also equipped with adjustable discharge rates, allowing operators to control the flow of powder according to specific process requirements. Additionally, the systems are designed for easy maintenance, with accessible components that can be serviced without extensive downtime. This feature contributes to higher overall equipment effectiveness (OEE) and lower operational costs.
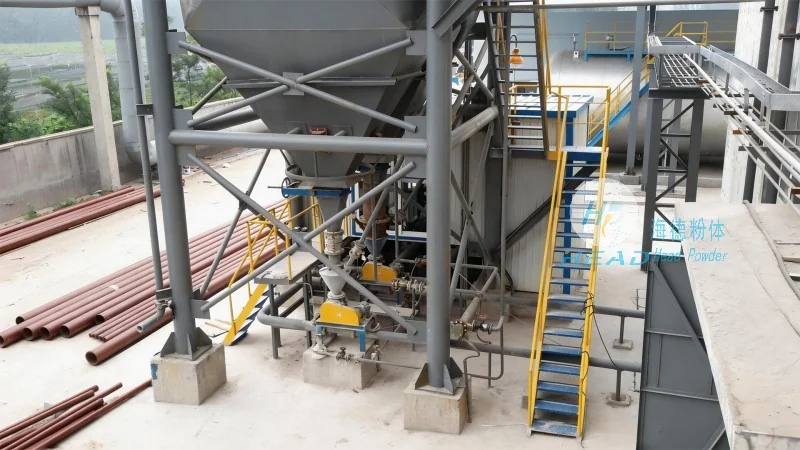
Technical Advantages and Application Scenarios
The technical design of headpowder's tonne bag unloading powder conveyors offers several advantages that make them ideal for diverse industrial settings. For instance, the use of robust materials, such as stainless steel or corrosion-resistant alloys, ensures durability and resistance to harsh chemical environments, which is particularly important in chemical and mining industries. The conveyors are also equipped with advanced sensors and control systems that monitor the bag's weight, the flow rate, and the system's operational status, providing real-time data for process optimization. These features help in maintaining consistent product quality and reducing waste. In terms of application scenarios, these conveyors are widely used in sectors like chemical manufacturing, where they handle raw materials like pigments and additives; in food processing, for transporting ingredients like flour and sugar; and in pharmaceutical production, for handling active pharmaceutical ingredients (APIs) and excipients. The versatility of the system allows it to adapt to different bag sizes and powder types, making it a reliable solution for bulk material handling across various industries.




