Working Principle and Features of Rare Earth Powder Conveying Systems
Release time:2026-09-17 10:01:22
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industries dealing with rare earth powders, efficient and reliable material handling is crucial to maintain production efficiency and product quality. The rare earth powder conveying system, developed by Shandong HeadPowder Engineering Co., Ltd. (commonly known as headpowder), is engineered to address the unique challenges of transporting these specialized materials. This article explores the working principle and key features of such systems, providing insights into their design and operational advantages.
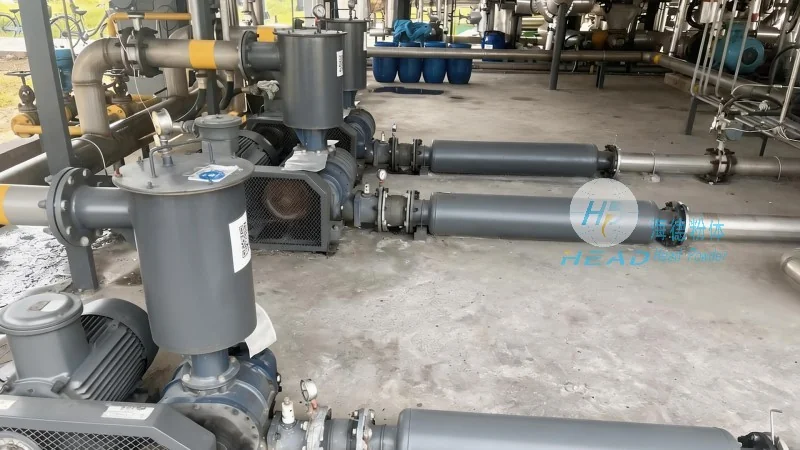
Working Principle of Rare Earth Powder Conveying Systems
The core of a rare earth powder conveying system lies in its ability to transport fine powders without causing agglomeration, contamination, or loss. Typically, these systems utilize a combination of mechanical components and specialized materials to ensure safe and efficient movement. The process generally involves several key steps:
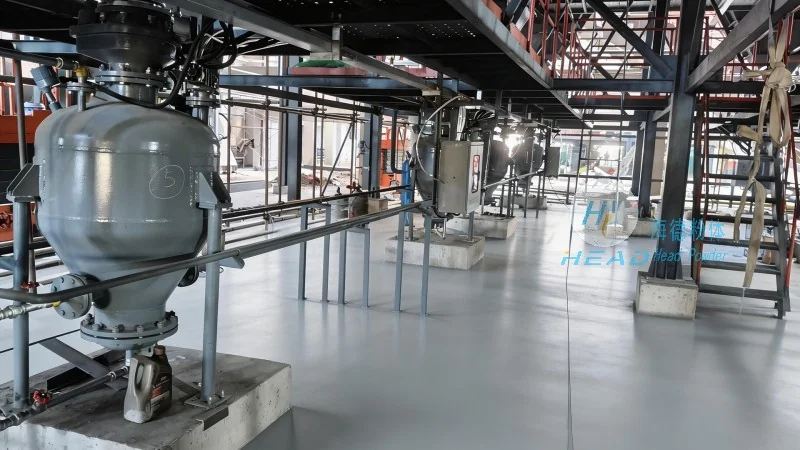
- Feeding and Metering: The system starts with the controlled feeding of rare earth powder from a storage hopper or silo. Precision feeders, such as screw feeders or rotary valves, regulate the flow rate to maintain consistent material delivery. This step is critical to prevent overloading or underloading, which can affect downstream processes.
- Conveying Mechanism: Once metered, the powder is transferred through a conveying tube or pipe. The most common methods include pneumatic conveying (using air pressure) and mechanical conveying (using screws, belts, or rollers). Pneumatic systems are particularly effective for fine powders, as they minimize particle breakage and maintain a consistent flow. Mechanical conveyors, on the other hand, are suitable for bulk materials and can handle higher capacities.
- Control and Monitoring: Advanced control systems monitor the entire process, adjusting parameters like air pressure, feed rate, and conveyor speed in real-time. Sensors and indicators ensure that any deviations from the set parameters are immediately detected, allowing for quick corrective actions. This level of automation enhances system reliability and reduces downtime.
Key Features of Rare Earth Powder Conveying Systems
Shandong HeadPowder Engineering Co., Ltd. designs rare earth powder conveying systems with several distinct features that set them apart in the industry. These features are tailored to meet the specific demands of handling rare earth materials, which are often sensitive and valuable.
- Material Compatibility: The components of the system are constructed from materials that are resistant to corrosion and wear caused by rare earth powders. Common materials include stainless steel, PTFE, and special alloys, ensuring that the powder does not react with or damage the equipment. This feature extends the system's lifespan and maintains the purity of the material.
- Low Particle Loss and Contamination: The design minimizes the risk of material loss during transport. Sealed systems and proper sealing of components prevent dust emissions and cross-contamination. This is vital for maintaining the quality of rare earth powders, which are often used in high-purity applications like electronics and magnets.
- Energy Efficiency: Modern conveying systems are engineered to operate with minimal energy consumption. By optimizing air pressure and conveyor speed, the system reduces operational costs while maintaining performance. This feature aligns with sustainability goals and contributes to lower overall production expenses.
- Customization and Scalability: Each system is customized to meet the specific requirements of the client, including material type, flow rate, and system size. The modular design allows for easy expansion or modification as production needs change. This flexibility ensures that the system remains effective and efficient over the long term.
Benefits of Using a Rare Earth Powder Conveying System
Implementing a rare earth powder conveying system offers numerous benefits for businesses involved in the processing and handling of rare earth materials. These advantages extend beyond mere material transport to include improved operational efficiency and cost savings.
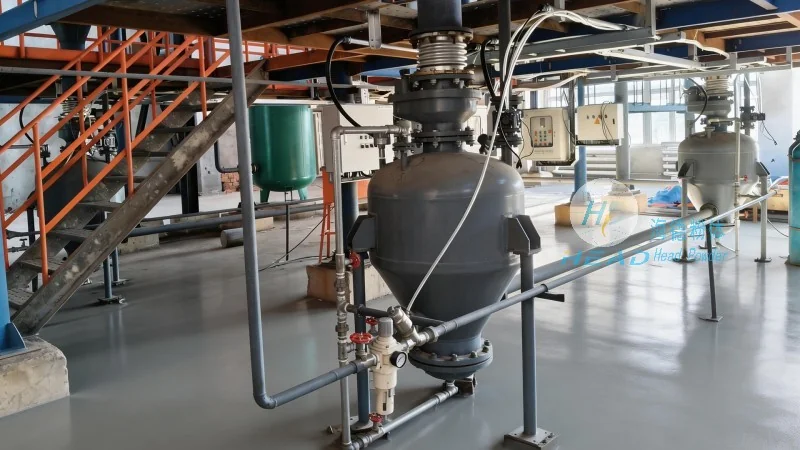
- Increased Production Efficiency: By automating the material handling process, the system reduces the need for manual labor and minimizes downtime. Consistent and reliable material delivery ensures that production lines operate smoothly, leading to higher output and reduced bottlenecks.
- Enhanced Product Quality: The system's design minimizes particle degradation and contamination, preserving the purity and quality of the rare earth powder. This is particularly important for applications where even minor impurities can affect performance, such as in the manufacturing of permanent magnets or electronic components.
- Cost Reduction: The energy-efficient operation and reduced maintenance requirements lower long-term costs. Additionally, the system's durability and low particle loss reduce the need for frequent replacements or repairs, further contributing to cost savings.
- Improved Safety: The sealed and enclosed design of the system prevents dust emissions and reduces the risk of inhalation or exposure to hazardous materials. This enhances workplace safety and complies with environmental regulations, providing peace of mind for both employees and management.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides advanced rare earth powder conveying systems that combine innovative technology with robust design. By understanding the working principle and key features of these systems, businesses can make informed decisions about their material handling solutions. The benefits of using such systems, including increased efficiency, improved product quality, and cost savings, make them an essential investment for any operation dealing with rare earth powders. With a focus on customization and reliability, headpowder continues to be a leader in providing solutions that meet the evolving needs of the industry.




