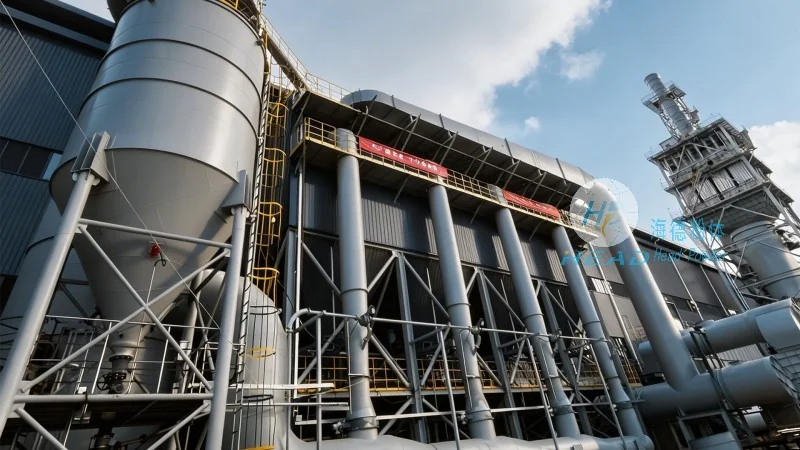
Quartz stone powder, a key material in various industrial applications, requires efficient and reliable transportation systems to ensure smooth production processes. The quartz stone powder conveying system equipment is a specialized solution designed to handle the unique properties of quartz stone powder, such as its fine particle size and abrasive nature. This article explores the components and design principles of such systems, highlighting their importance in industrial operations.
Introduction to Quartz Stone Powder Conveying Systems
Quartz stone powder, derived from natural quartz rock, is widely used in industries like construction, electronics, and cosmetics due to its high purity and durability. However, its fine particle size and abrasive characteristics make traditional conveying methods inefficient and potentially damaging to equipment. The quartz stone powder conveying system equipment addresses these challenges by providing a controlled and safe method for transporting the powder from one location to another within a production facility. These systems are essential for maintaining product quality and operational efficiency in industries that rely on quartz stone powder.
Key Components of Quartz Stone Powder Conveying Systems
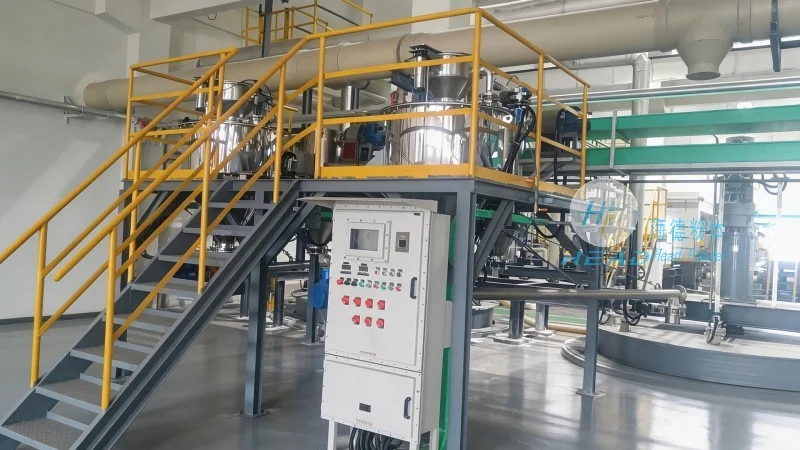
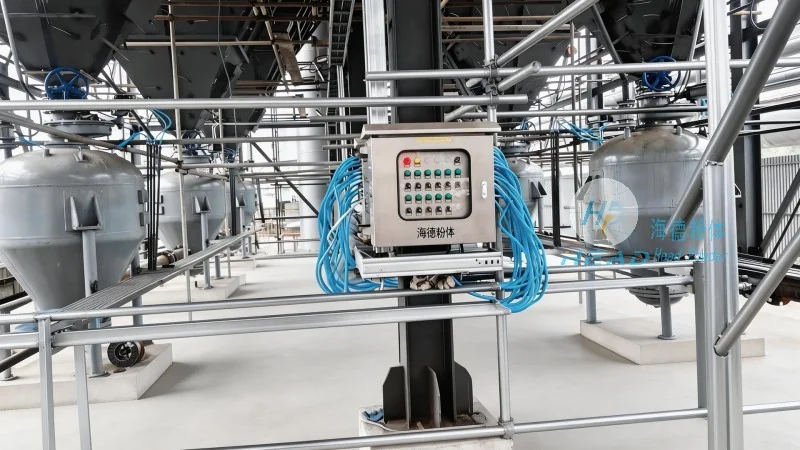
The quartz stone powder conveying system typically consists of several key components that work together to ensure effective material handling. The primary components include a hopper for material storage, a feeding mechanism to control the flow of powder, a conveying device (such as a screw conveyor or pneumatic conveyor), and a control system to regulate the entire process. The hopper is designed to accommodate the bulk storage of quartz stone powder, often with a conical or rectangular shape to facilitate uniform material discharge. The feeding mechanism, usually a rotary valve or a gate valve, ensures a consistent and controlled flow of powder into the conveying device. The conveying device is the core of the system, responsible for transporting the powder through the system. Screw conveyors are commonly used for horizontal or slightly inclined transport, while pneumatic conveyors are ideal for vertical or long-distance transport due to their ability to handle fine powders without clogging. The control system, often integrated with sensors and automation technology, monitors the flow rate, pressure, and other parameters to maintain optimal performance and prevent system failures.
Design Principles Behind Quartz Stone Powder Conveying Systems
The design of quartz stone powder conveying systems is based on several fundamental principles to ensure efficiency, reliability, and safety. The first principle is the consideration of the material's physical properties, such as particle size distribution, density, and abrasiveness. These properties dictate the choice of conveying equipment and the system's overall design. For example, fine quartz stone powder may require a pneumatic conveyor to avoid particle segregation and clogging, while larger particles might be better suited for screw or belt conveyors. The second principle is the application of fluid dynamics and mechanical engineering principles to optimize the conveying process. This includes calculating the required air velocity or screw speed to achieve the desired flow rate while minimizing energy consumption. The third principle is the integration of safety features to protect both the equipment and personnel. This includes dust collection systems to prevent airborne particle exposure, explosion-proof designs for hazardous environments, and emergency stop mechanisms to ensure quick response in case of system malfunctions. Additionally, the design considers the system's scalability and adaptability to accommodate future production needs or changes in material specifications.
Role of Shandong HeadPowder Engineering Co., Ltd. in Quartz Stone Powder Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality quartz stone powder conveying systems. With years of experience and a commitment to innovation, the company provides tailored solutions that meet the specific needs of its clients. The company's products are engineered to handle the unique challenges of quartz stone powder, ensuring efficient and reliable operation. By leveraging advanced technology and rigorous quality control, Shandong HeadPowder Engineering Co., Ltd. delivers systems that enhance productivity, reduce maintenance costs, and improve overall operational efficiency. The company's expertise in material handling and industrial engineering allows it to develop customized solutions that integrate seamlessly with existing production lines, providing a competitive edge to its clients in various industries.
Conclusion
In conclusion, quartz stone powder conveying systems are critical components in industries that rely on quartz stone powder for their operations. The design and implementation of these systems require careful consideration of the material's properties and the application's requirements. By understanding the key components and design principles, industries can select and operate effective conveying systems that enhance productivity and ensure product quality. Shandong HeadPowder Engineering Co., Ltd. plays a vital role in this field, providing reliable and efficient solutions that meet the evolving needs of the industry.




