This equipment is a specialized solution designed to handle bulk powder materials, particularly those delivered in bags. The system integrates a bag breaker mechanism with a conveying unit, enabling seamless transfer of powders from bags to storage or processing facilities. Such systems are crucial in industries like pharmaceuticals, chemicals, food processing, and more, where handling bulk powders efficiently and safely is paramount.
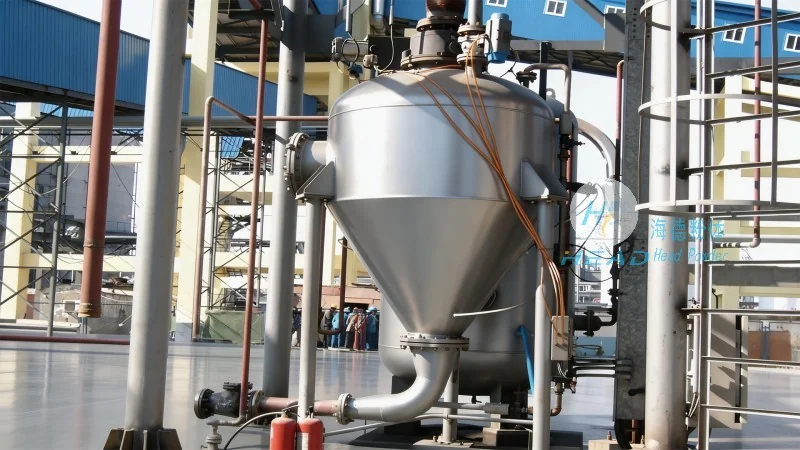
Understanding the Equipment's Core Function
The primary function of a bag breaker powder conveying system is to automate the process of opening bags, emptying their contents, and transporting the powder to the next stage of production or storage. This eliminates manual labor, reduces the risk of dust exposure, and enhances operational efficiency. The system typically consists of a hopper or receiving chamber that captures the bag, a bag opening mechanism (like a knife or impact device), and a conveyor system that moves the material to a silo, tank, or processing line.
Design Principles Behind the System
The design of a bag breaker powder conveying system is guided by several key principles to ensure reliability, efficiency, and safety. First, the system must be robust enough to handle various bag sizes and materials without damage. Second, the bag opening mechanism must be precise and gentle to avoid contaminating the powder. Third, the conveying component should maintain the integrity of the powder, preventing segregation or degradation. Fourth, the entire system is designed for easy maintenance and cleaning, which is critical in industries with strict hygiene standards.
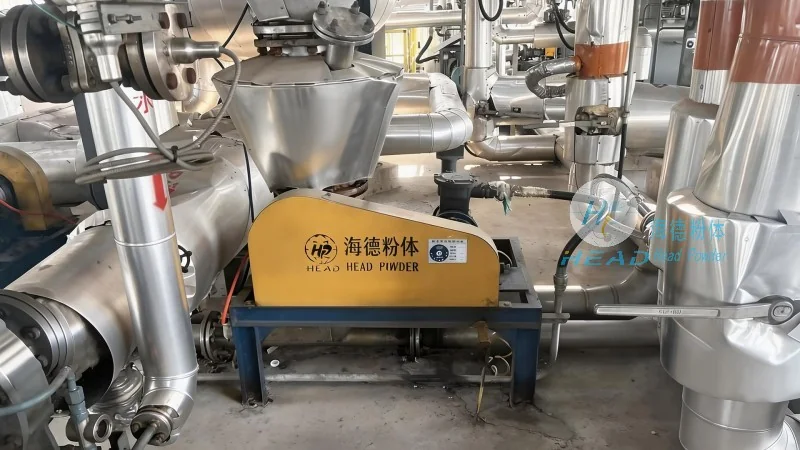
Key Components and Their Roles
Several critical components make up a bag breaker powder conveying system. The bag receiving hopper is the first component, designed to securely hold the bag in place. The bag opening mechanism, which may include a rotating knife or impact plate, is responsible for cutting or breaking the bag open. The powder transfer section, often a screw conveyor or pneumatic system, moves the material from the hopper to the destination. The control system manages the entire process, ensuring each step is executed in sequence and safely. Each component is engineered to work in harmony, optimizing the overall performance of the system.
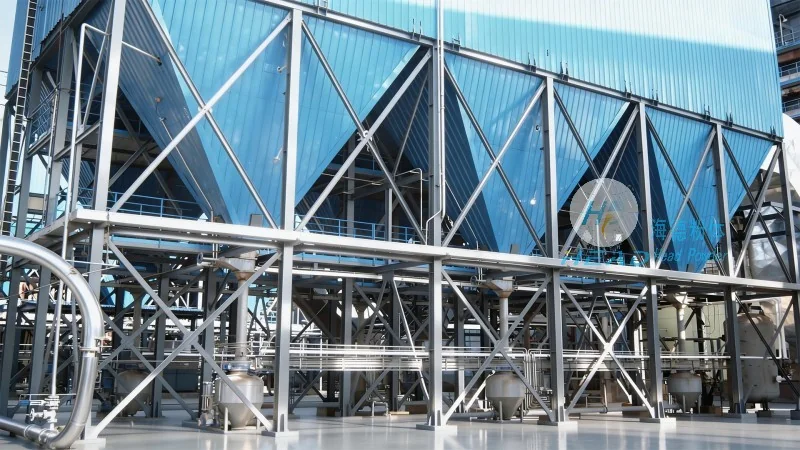
Application Scenarios and Benefits
Bag breaker powder conveying systems are widely used in various industrial applications. In the pharmaceutical industry, they ensure the safe and hygienic transfer of active pharmaceutical ingredients (APIs) and excipients. In the chemical sector, they handle raw materials like pigments, catalysts, and solvents. The food industry uses them for processing ingredients like flour, sugar, and spices. The key benefits include increased productivity, reduced labor costs, improved safety by minimizing dust exposure, and enhanced product quality through consistent handling. These systems also contribute to a cleaner and more organized production environment.
Company Information and Contact Details
The equipment is manufactured by Shandong HeadPowder Engineering Co., Ltd., a leading company in the field of powder handling solutions. HeadPowder specializes in designing and producing high-quality bag breaker powder conveying systems tailored to meet the specific needs of different industries. The company is located in Shandong, China, and is committed to providing reliable, efficient, and safe solutions for bulk powder handling. For more information or to inquire about their products, interested parties can contact the company directly.




