For industrial applications that require efficient and reliable material handling, the glass fiber pneumatic conveying system stands out as a sophisticated solution. This technology is designed to transport bulk materials through a pipeline using air or other gas as the conveying medium. The system is particularly valued for its ability to handle a wide range of materials, including those that are abrasive, dusty, or sensitive to moisture, making it suitable for various industries such as pharmaceuticals, food processing, and chemical manufacturing.
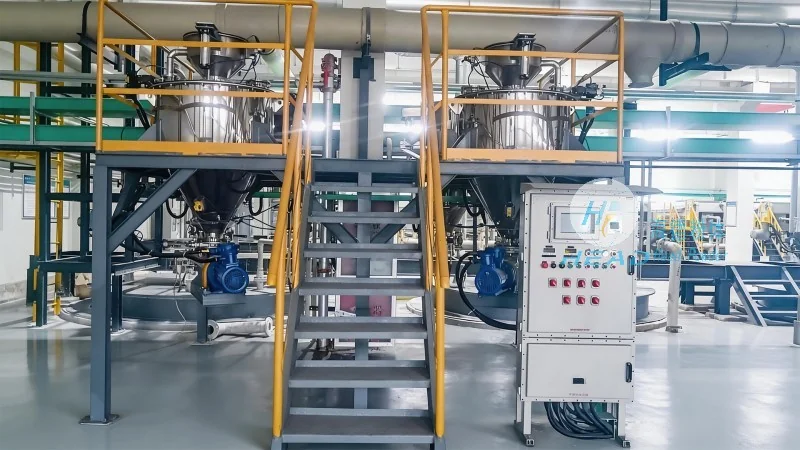
Understanding the Glass Fiber Pneumatic Conveying System
The core of a glass fiber pneumatic conveying system is the use of a flexible, yet durable, glass fiber hose or tube to transport materials. This material choice is critical because it offers exceptional resistance to chemical corrosion, high temperatures, and mechanical wear, ensuring long-term performance and minimal maintenance. The system operates by creating a pressure differential, either through suction (negative pressure) or pressure (positive pressure), to move the material from the source to the destination. The design allows for gentle material handling, reducing product degradation and preserving the integrity of the conveyed items.
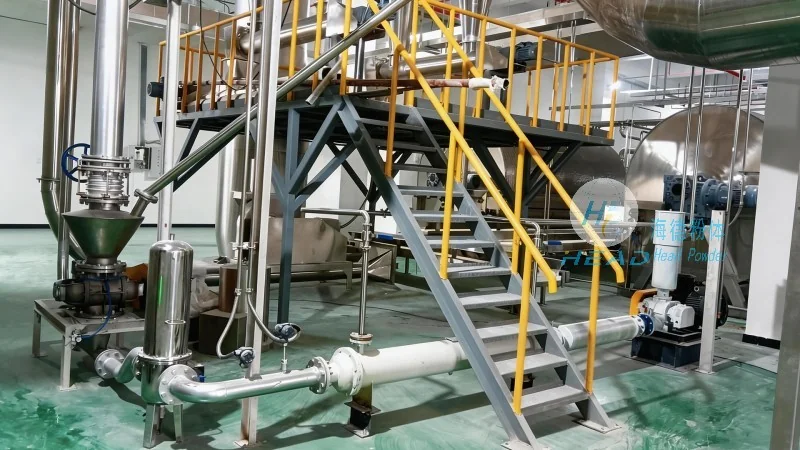
Key Design Principles of the System
Several fundamental design principles govern the effective operation of a glass fiber pneumatic conveying system. First, the system must be tailored to the specific characteristics of the material being conveyed, such as particle size, density, and flowability. This involves selecting the appropriate air velocity and pressure to ensure smooth transport without causing blockages or excessive wear. Second, the system incorporates a series of components, including a hopper for material loading, a venturi or air lock for air-material mixing, and a receiver for material discharge. Each component is engineered to work in harmony, optimizing the conveying process and minimizing energy consumption. Third, the design emphasizes safety and compliance with industrial standards, ensuring that the system operates within safe pressure and temperature limits and adheres to relevant regulations for material handling.
Applications and Benefits
The glass fiber pneumatic conveying system finds extensive application in industries where traditional conveying methods, such as belt conveyors or bucket elevators, are less suitable. For instance, in the pharmaceutical industry, the system’s ability to handle sensitive powders without contamination is invaluable. In food processing, the system’s hygienic design and resistance to cleaning agents make it a preferred choice. The benefits of this technology extend beyond material handling efficiency; it also reduces labor costs by automating the transport process and minimizes the risk of material spillage or exposure to personnel. Additionally, the system’s compact design allows for installation in spaces where traditional equipment may not fit, making it a versatile solution for modern industrial settings.
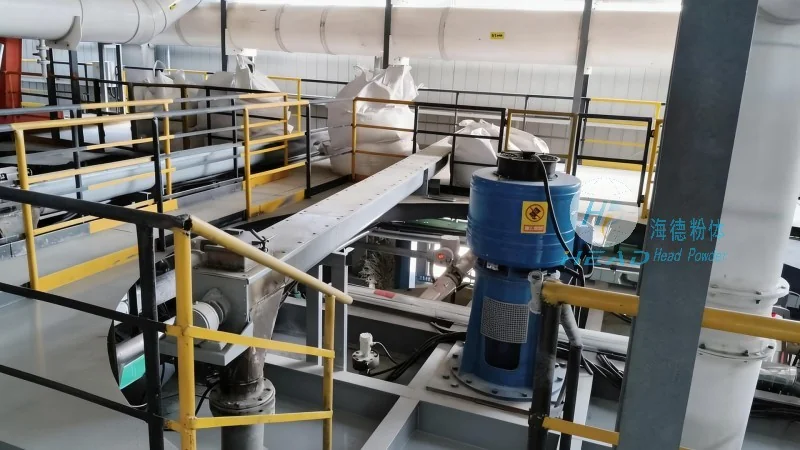
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and producing glass fiber pneumatic conveying systems tailored to the unique needs of its clients. HeadPowder’s commitment to using high-quality materials, such as durable glass fiber hoses, ensures that its products deliver long-lasting performance and reliability. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge solutions for global markets. By combining technical expertise with customer-centric service, HeadPowder has established itself as a trusted partner in the material handling industry, providing solutions that enhance operational efficiency and product quality.




