

Calculation and Equipment Selection for Air-Driven Limestone Powder Conveying
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, calculation, and equipment selection for air-driven limestone powder conveying systems. With a strong focus on industrial efficiency and material handling solutions, the company provides comprehensive services tailored to the unique needs of various industries.
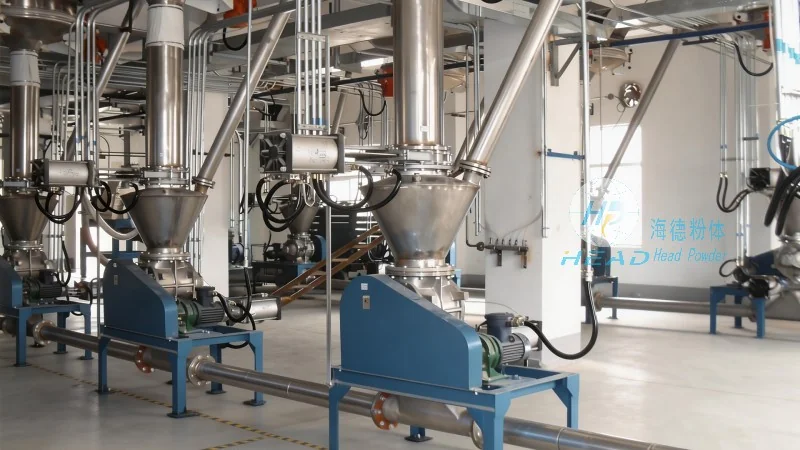
Understanding Air-Driven Limestone Powder Conveying Systems
Limestone powder, a critical raw material in numerous industrial processes, requires reliable and efficient transportation methods to ensure smooth operations. Air-driven conveying systems offer a viable solution by utilizing compressed air to transport dry powders like limestone over long distances with minimal maintenance. These systems are particularly advantageous in environments where traditional mechanical conveyors may face challenges due to dust, moisture, or material abrasiveness.
Key Design Calculations for Limestone Powder Conveying
The successful implementation of an air-driven limestone powder conveying system relies on precise design calculations. These calculations involve determining several critical parameters to ensure optimal performance and system longevity. The primary considerations include material flow rate, air velocity, pressure drop, and system power requirements. Engineers at HeadPowder employ advanced methodologies to analyze the physical properties of limestone powder, such as particle size distribution, bulk density, and flowability, to tailor the system design accordingly.
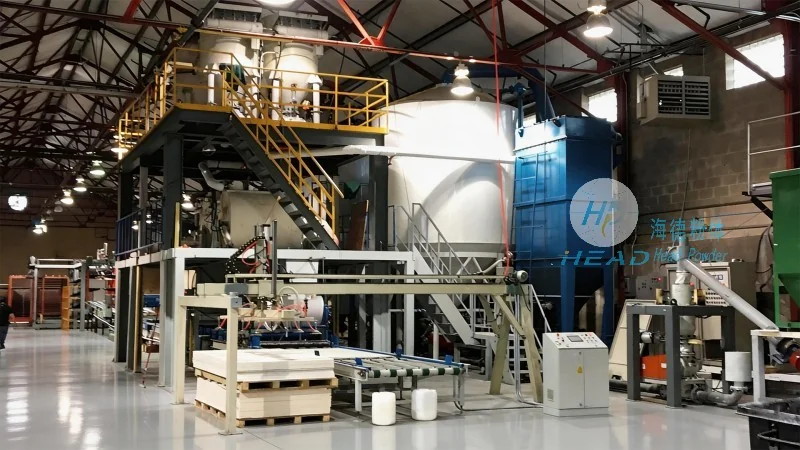
One of the core calculations is determining the required air velocity to achieve reliable powder transport. This involves assessing the minimum velocity needed to prevent material settling in the pipeline and the maximum velocity to avoid excessive wear on components. The pressure drop across the system is another crucial factor, as it directly impacts energy consumption and the overall system efficiency. By accurately modeling the pipeline layout, including bends, elbows, and expansion joints, engineers can predict the pressure losses and optimize the system for minimal energy use.
Equipment Selection for Air-Driven Limestone Powder Conveying
HeadPowder offers a range of specialized equipment designed to meet the specific demands of limestone powder conveying applications. The selection process is based on a thorough analysis of operational requirements, material characteristics, and environmental factors. Key equipment includes rotary air locks, which act as airlocks to prevent backflow and maintain consistent material flow; filter units to capture and recycle fine particles, ensuring compliance with air quality regulations; and pressure vessels or silos for material storage and feeding.
The company’s engineers evaluate various components, such as blowers or compressors, to determine the most suitable air supply source. Centrifugal blowers are commonly used for high-volume applications due to their ability to handle large air volumes with lower pressure, while positive displacement blowers may be preferred for applications requiring higher pressure. The choice of pipeline material, typically stainless steel or PVC, is also critical to prevent corrosion and ensure durability in the presence of limestone dust and moisture.
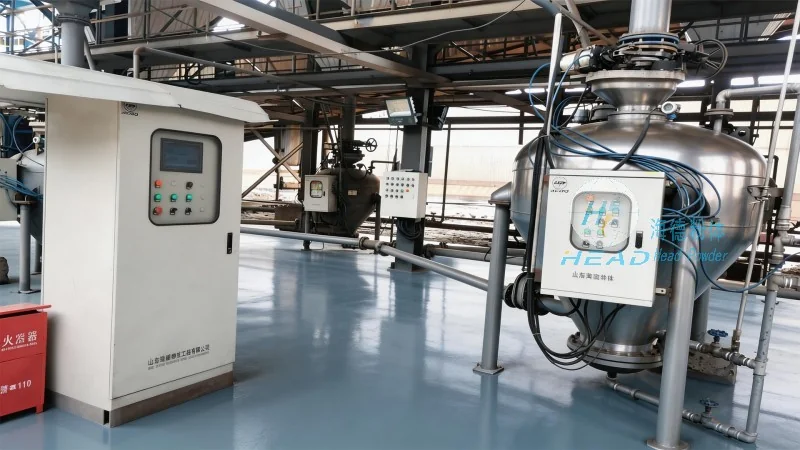
Customized Solutions from HeadPowder Engineering
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, leverages its extensive experience in industrial engineering to deliver customized air-driven limestone powder conveying solutions. The company’s team of experts works closely with clients to understand their operational challenges and design systems that maximize efficiency, reduce downtime, and minimize maintenance costs. By integrating advanced design software and real-world testing, HeadPowder ensures that each project meets the highest standards of performance and reliability.
Whether for new installations or upgrades to existing systems, HeadPowder provides comprehensive support, from initial feasibility studies to final commissioning and ongoing maintenance services. The company’s commitment to quality and customer satisfaction has established it as a trusted partner in the material handling industry, serving clients across various sectors including chemical, pharmaceutical, and food processing.