The rice husk ash powder conveying system is a specialized equipment designed for the efficient and reliable transportation of rice husk ash, a byproduct commonly used in various industrial applications such as cement production, fertilizer manufacturing, and environmental remediation. This system is engineered to handle the unique properties of rice husk ash, including its fine particle size, lightweight nature, and potential for dust generation, ensuring safe and effective material handling throughout the process.
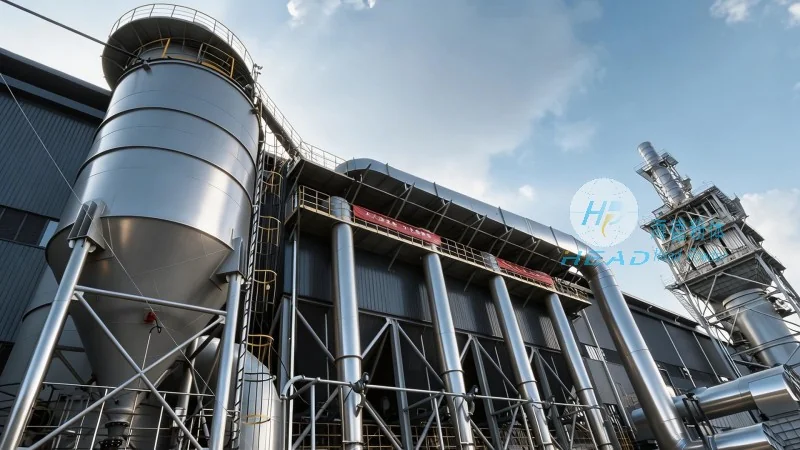
Company Overview
HeadPowder, a leading provider in the field of powder handling technology, is the manufacturer behind this advanced conveying system. As Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, the company specializes in developing and supplying high-quality equipment for powder processing, with a strong focus on innovation and customer-centric solutions. The company's expertise in material handling systems has enabled it to create reliable solutions that meet the diverse needs of industrial clients.
System Structure Overview
The rice husk ash powder conveying system comprises several key components that work in tandem to ensure smooth operation. The primary components include a hopper for material storage, a feeding mechanism to control the flow of ash into the system, a conveying pipe network that transports the powder, and a control system for monitoring and regulating the process. The hopper is typically designed with a sloped bottom to facilitate material discharge, while the feeding mechanism may utilize screw conveyors or rotary valves to ensure consistent and controlled feeding. The conveying pipe network is often made of durable materials like stainless steel or PVC to withstand the abrasive nature of the ash particles and prevent material buildup or corrosion. Additionally, the system may include dust collection and filtration components to maintain air quality and comply with environmental regulations.
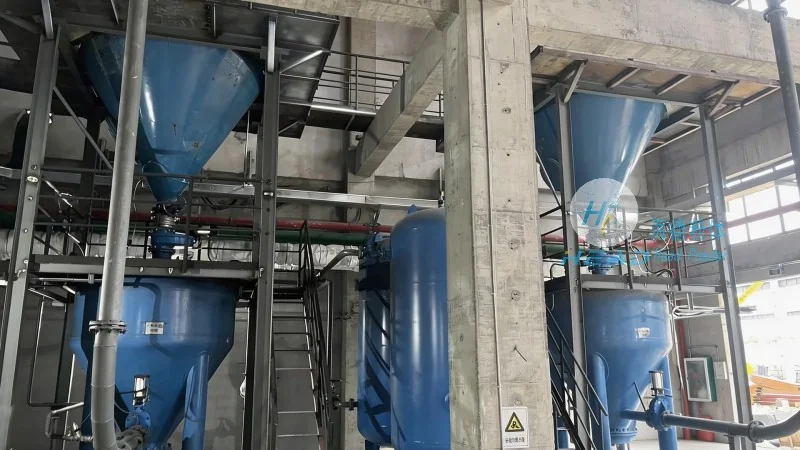
Working Principles of the Conveying System
The operation of the rice husk ash powder conveying system follows a systematic process that ensures efficient material transport. Initially, rice husk ash is fed into the hopper from the source material storage area. The feeding mechanism then regulates the flow of ash into the conveying pipe, which is driven by a motorized pump or fan system. The conveying medium, such as air or a combination of air and mechanical force, moves the ash particles through the pipe network. The control system continuously monitors parameters like pressure, flow rate, and temperature to maintain optimal operation and prevent system failures. The system is designed to handle varying ash loads and particle sizes, ensuring consistent performance even under fluctuating conditions. The final stage involves delivering the ash to the target destination, such as a processing plant or storage silo, where it can be further utilized in downstream applications.
Technical Features and Advantages
The rice husk ash powder conveying system offers several technical advantages that make it an ideal choice for industrial applications. One of the key features is its high efficiency in material transport, with the ability to handle large volumes of ash at a consistent rate. The system is also designed for low maintenance, with components that are easy to access and replace, reducing downtime and operational costs. Additionally, the system incorporates advanced safety features, such as dust suppression and explosion-proof designs, to ensure safe operation in environments where dust is a potential hazard. The use of durable materials and robust construction ensures long-term reliability and minimal wear and tear, extending the system's service life. Furthermore, the system's modular design allows for easy customization and integration with existing industrial setups, providing flexibility for different production requirements.
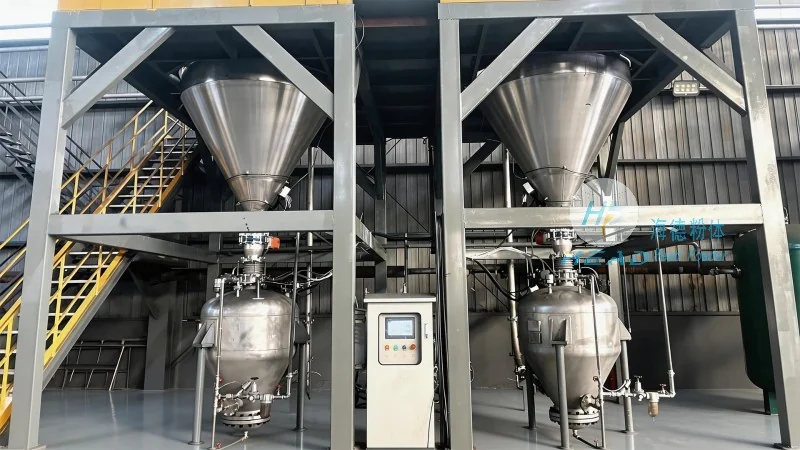
Application and Integration
The rice husk ash powder conveying system is widely used in various industrial sectors where rice husk ash is a critical raw material. In the cement industry, for example, the system efficiently transports ash to the mixing plants, where it is used as a supplementary cementitious material to improve the properties of concrete. In the fertilizer industry, the system delivers ash to processing facilities, where it is incorporated into nutrient-rich products. The system's adaptability also makes it suitable for environmental remediation projects, where ash is used in soil stabilization or waste treatment processes. The integration of the system with existing production lines is straightforward, as it can be connected to existing hoppers, silos, or processing equipment without significant modifications. This ensures seamless operation and minimal disruption to ongoing production activities.
Conclusion
In summary, the rice husk ash powder conveying system is a sophisticated and reliable solution for the efficient handling of rice husk ash. Developed by Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, the system combines advanced engineering with robust construction to meet the demanding requirements of industrial applications. Its structured design, efficient working principles, and technical advantages make it an essential component for industries relying on rice husk ash as a valuable resource. The system's ability to handle varying conditions and maintain consistent performance ensures that clients can rely on it for long-term operational success.




