Cement aggregate material handling systems are essential components in the construction and industrial sectors, designed to efficiently transport and manage bulk materials such as cement, aggregates, and other raw materials. These systems play a crucial role in optimizing production processes, enhancing operational efficiency, and ensuring the smooth flow of materials from storage to processing units. Understanding the working principle and key features of such systems is vital for industries aiming to streamline their material handling operations.
Working Principle of Cement Aggregate Material Handling Systems
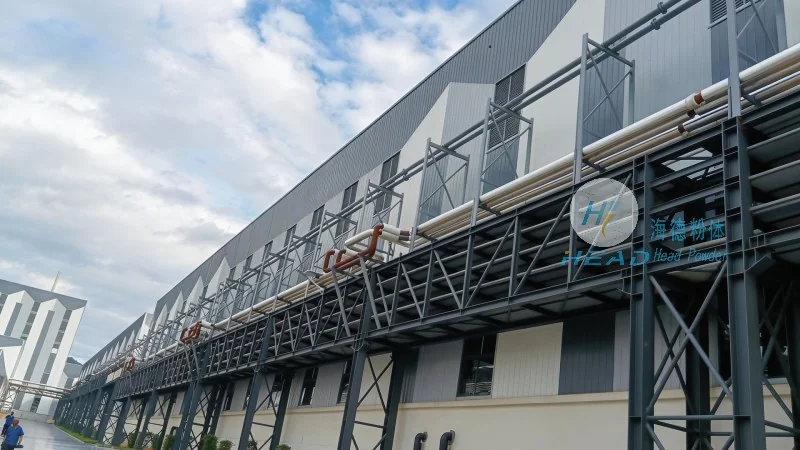
The working principle of cement aggregate material handling systems typically involves a combination of mechanical and hydraulic components that work in tandem to move materials. Common mechanisms include conveyor belts, screw conveyors, bucket elevators, and pneumatic conveying systems. Each component is engineered to handle specific material types and operational requirements. For instance, conveyor belts are widely used for horizontal and slight incline transport, while screw conveyors are ideal for vertical or inclined movement. Bucket elevators are particularly effective for vertical lifting of heavy aggregates, and pneumatic systems utilize air pressure to transport fine powders like cement. The system's control panel allows operators to adjust speed, direction, and load capacity, ensuring precise material handling. This integrated approach ensures that materials are moved safely, efficiently, and with minimal loss or contamination.
Key Features of Cement Aggregate Material Handling Systems
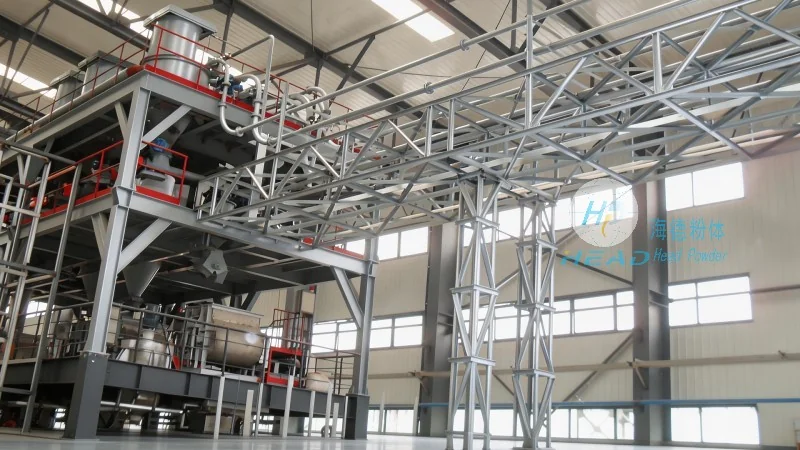
Cement aggregate material handling systems are characterized by several key features that enhance their performance and usability. One of the primary features is their high capacity and durability, designed to handle large volumes of materials with minimal maintenance. These systems are constructed from robust materials such as stainless steel and heavy-duty plastics, ensuring resistance to wear, corrosion, and impact. Another significant feature is their adaptability, as they can be customized to suit various industrial applications, including concrete mixing plants, asphalt production facilities, and mining operations. The systems also incorporate advanced safety features, such as overload protection, emergency stop buttons, and automatic shut-off mechanisms, to prevent accidents and ensure operator safety. Additionally, modern systems often include monitoring and control technologies, allowing real-time tracking of material flow, energy consumption, and system performance. This data-driven approach enables proactive maintenance and optimization, reducing downtime and operational costs.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
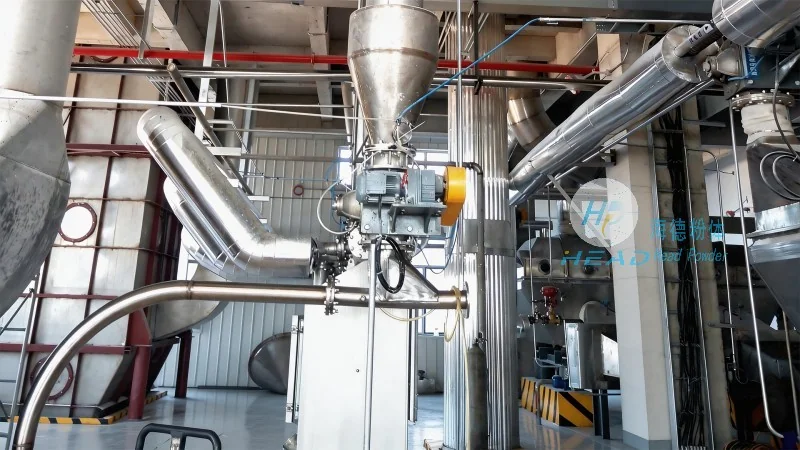
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-quality material handling systems for the cement and construction industries. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder specializes in designing, manufacturing, and installing customized cement aggregate material handling systems tailored to the specific needs of its clients. The company's commitment to quality, innovation, and customer satisfaction has earned it a reputation for excellence in the industry. By leveraging advanced engineering techniques and rigorous quality control processes, HeadPowder ensures that its products meet international standards and deliver superior performance in real-world applications. The company's team of experienced engineers and technicians works closely with clients to understand their operational requirements and develop solutions that enhance productivity and reduce costs. HeadPowder's focus on sustainability and energy efficiency is also a key aspect of its product design, as it strives to provide environmentally friendly solutions that contribute to the industry's long-term growth and development.
Conclusion
In conclusion, cement aggregate material handling systems are critical for optimizing material flow in construction and industrial operations. Their working principles, which combine mechanical and hydraulic components, enable efficient transport of bulk materials. The key features, including high capacity, durability, adaptability, and advanced safety and monitoring systems, make these systems indispensable for modern industrial applications. Shandong HeadPowder Engineering Co., Ltd. stands as a prominent provider in this field, offering customized solutions that meet the diverse needs of its clients. By understanding the working principles and features of these systems, industries can enhance their operational efficiency, reduce costs, and ensure the smooth progression of their material handling processes. As technology continues to advance, cement aggregate material handling systems will likely evolve to incorporate more intelligent and sustainable features, further improving their performance and contribution to industrial productivity.




