

What is a Tote Bag Unpacking Powder Material Handling System Equipment? What are its Design Principl
When it comes to handling bulk powder materials, especially those stored in large tote bags, efficient and reliable systems are essential for industrial operations. The tote bag unpacking powder material handling system equipment represents a specialized solution designed to streamline the process of transferring these materials from the storage container to the processing line. This equipment is widely used across various industries, including chemical manufacturing, food processing, pharmaceuticals, and more, where the safe and efficient movement of powders is critical.
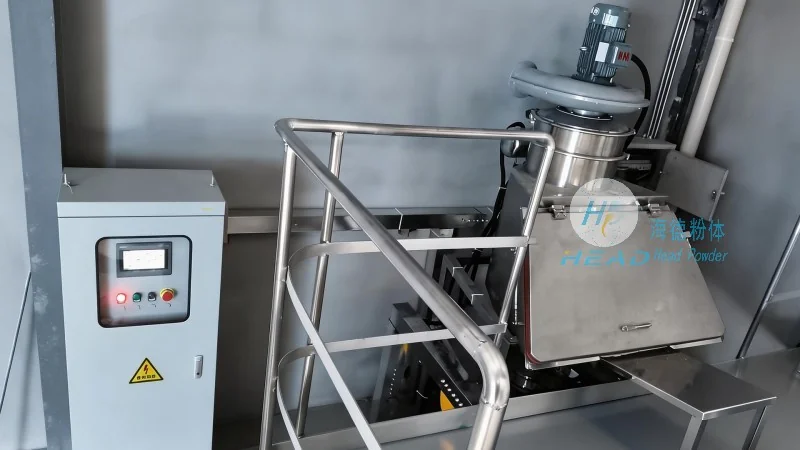
Understanding Tote Bag Unpacking Powder Material Handling Systems: An Overview
A tote bag, also known as a super sack or bulk bag, is a large, flexible container used to store and transport bulk materials. These bags are typically made of durable fabric and can hold significant quantities of powder, often ranging from several hundred to several thousand kilograms. The tote bag unpacking system is designed to automate the process of opening the bag, emptying its contents, and transferring the powder to a conveyor, silo, or other processing equipment. This automation reduces manual labor, minimizes material loss, and enhances safety by eliminating the need for workers to handle heavy or potentially hazardous bags.
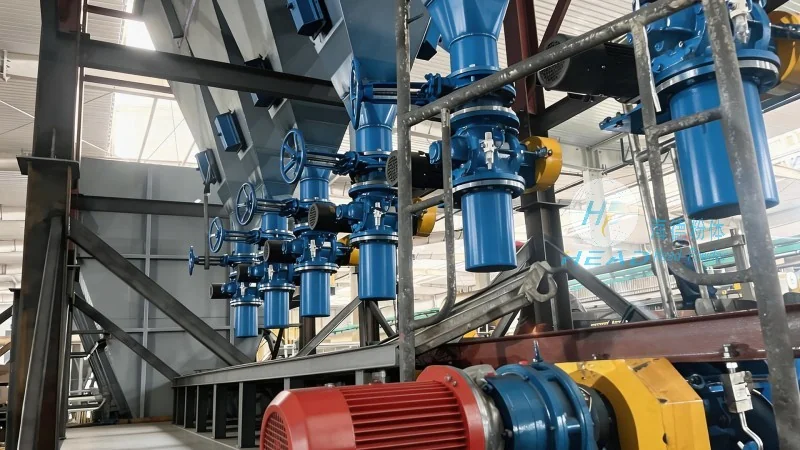
Key Components and Design Principles
The design of a tote bag unpacking powder material handling system is centered around several key components that work in concert to achieve efficient material transfer. The primary components include a bag opening mechanism, a discharge valve or spout, a conveyor system, and often a dust collection or filtration unit. The bag opening mechanism may involve a mechanical or pneumatic system to cut or tear the bag's top, while the discharge valve controls the flow of material from the bag into the conveyor. The conveyor system then transports the powder to the next stage of processing, such as a silo for storage or a mixer for blending. The design principles focus on maximizing throughput, minimizing downtime, and ensuring the safety of both the equipment and the operators. For instance, the system may incorporate features like automatic bag detection, which triggers the opening process once a bag is positioned correctly, and material flow control to prevent overloading or clogging of the conveyor.
The Role of Tote Bag Unpacking Systems in Material Handling
In industrial settings, the tote bag unpacking system plays a crucial role in maintaining operational efficiency and product quality. By automating the transfer of bulk powders, these systems reduce the time and labor required for manual handling, which can be both time-consuming and prone to errors. Additionally, the automated process helps maintain consistent material flow, which is vital for processes that require precise dosing or blending. The system also contributes to improved safety by minimizing exposure of workers to heavy bags and potential dust or particulate emissions. This is particularly important in industries where powders may be hazardous or where strict safety regulations are in place. Furthermore, the design of these systems often allows for integration with other material handling equipment, such as silos, mixers, or packaging lines, creating a seamless material flow from receipt to processing.
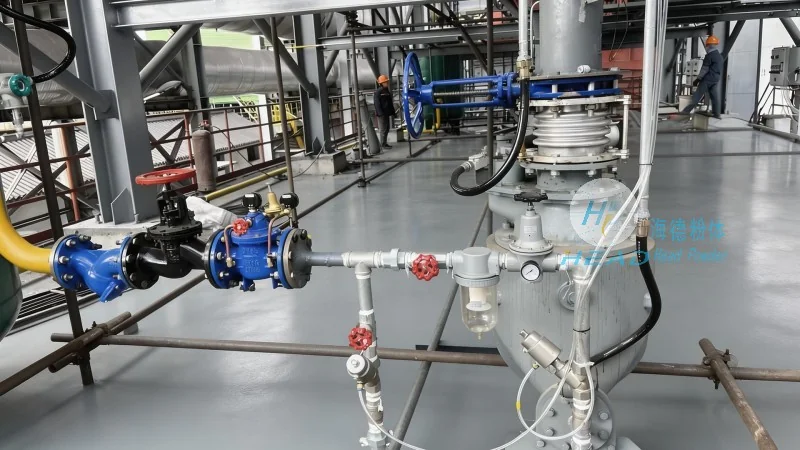
Shandong HeadPowder Engineering Co., Ltd.: Expert in Tote Bag Unpacking Systems
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and supply of advanced tote bag unpacking powder material handling systems. With years of experience in the industry, the company has developed systems that meet the diverse needs of various sectors, from chemical production to food processing. The company's approach emphasizes customization, ensuring that each system is tailored to the specific requirements of the client, including the type of powder, bag size, and processing capacity. The engineering team at HeadPowder leverages advanced technology and materials to create robust, reliable systems that offer high performance and durability. The company's facilities are located in Shandong, China, where they conduct research and development, manufacturing, and quality control to ensure that every product meets the highest standards. By choosing HeadPowder, clients benefit from a comprehensive solution that includes not only the equipment but also technical support and after-sales service, ensuring long-term operational efficiency and reliability.