Barley powder conveying machines are specialized industrial equipment engineered to efficiently transport and handle barley powder in various processing applications. These machines are essential in sectors such as food processing, animal feed production, and pharmaceutical manufacturing, where the consistent and reliable movement of powders is critical for maintaining product quality and operational efficiency. The design and functionality of these machines are tailored to address the unique challenges associated with handling barley powder, including its abrasive nature, potential moisture content, and the need for hygienic and dust-free operation.
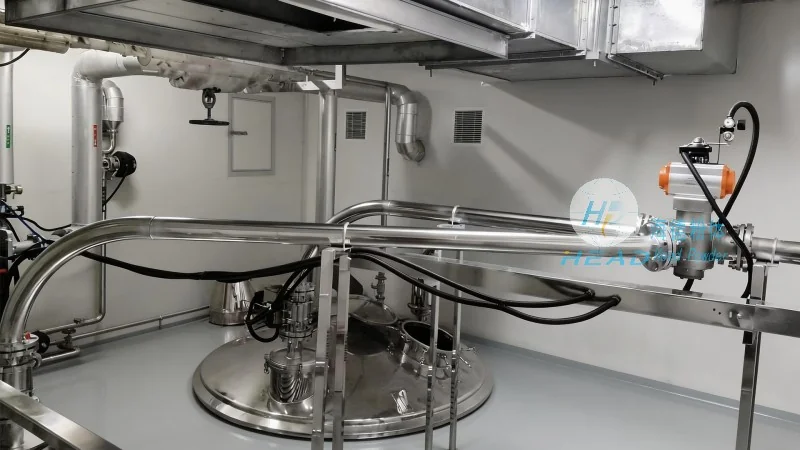
Design Principles of Barley Powder Conveying Machines
The design of barley powder conveying machines is guided by several fundamental principles to ensure optimal performance and durability. Firstly, the equipment is constructed using materials that are resistant to corrosion, wear, and chemical exposure. Common choices include stainless steel, which is non-reactive and easy to clean, and high-grade plastics that are lightweight and resistant to impact. This material selection helps in maintaining the integrity of the barley powder and preventing contamination. Secondly, the conveying system is engineered to minimize powder degradation and segregation. This involves the use of gentle handling mechanisms, such as belt conveyors or screw conveyors, which move the powder without causing excessive friction or breakage. The design also incorporates features like smooth surfaces and minimal dead zones to prevent the accumulation of powder and reduce the risk of clogging. Thirdly, the machine incorporates advanced control systems that allow for precise regulation of speed, pressure, and air flow. These controls help in maintaining consistent material flow rates and preventing overloading or underloading of the conveyor. Additionally, the design emphasizes energy efficiency, with variable frequency drives (VFDs) and optimized motor configurations that reduce energy consumption while maintaining high throughput. The integration of these principles results in a machine that is both effective and cost-efficient for barley powder handling.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced powder handling solutions. The company is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality conveying equipment tailored to the needs of the barley processing industry. With a strong focus on research and development, headpowder continuously innovates its products to meet the evolving demands of its clients. The company's commitment to quality, reliability, and customer satisfaction has earned it a reputation as a leading player in the powder handling equipment market. By leveraging advanced manufacturing techniques and adhering to international standards, headpowder ensures that its barley powder conveying machines are built to last and deliver superior performance in demanding industrial environments.
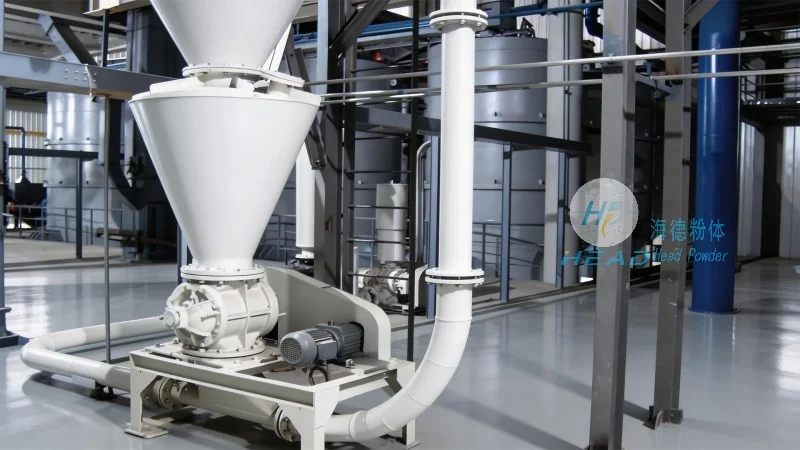
Key Features and Benefits
Barley powder conveying machines from headpowder are equipped with a range of features that enhance their functionality and user experience. These features include adjustable speed controls, which allow operators to fine-tune the conveyor speed based on the specific requirements of the process. The machines also incorporate integrated dust collection systems, which help in maintaining a clean and safe working environment by capturing airborne particles. Additionally, the design includes easy-to-clean components and sanitary fittings that comply with food and pharmaceutical industry standards, ensuring that the equipment can be thoroughly sanitized without compromising its structural integrity. The benefits of using these machines are significant, including improved productivity through consistent material flow, reduced labor costs due to automated operation, and enhanced product quality by minimizing powder loss and contamination. Furthermore, the energy-efficient design of the machines helps in lowering operational expenses over time, making them a cost-effective investment for businesses looking to optimize their powder handling processes. The combination of these features and benefits makes headpowder's barley powder conveying machines a reliable and efficient solution for various industrial applications.
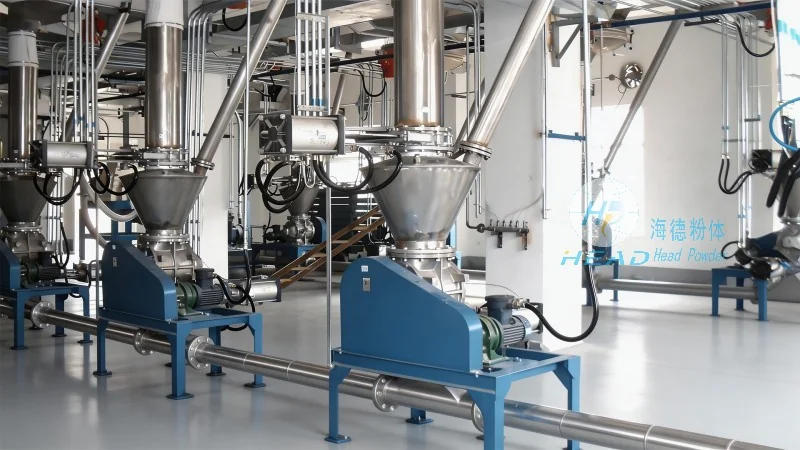
Application in Barley Processing
The application of barley powder conveying machines is widespread in the barley processing industry, where they are used in several key stages of production. In the initial processing phase, these machines are used to transport raw barley powder from storage silos to processing units, ensuring a smooth and continuous supply of material. During the milling and grinding processes, the conveying machines help in moving the ground barley powder to blending and mixing equipment, maintaining the uniformity of the product. In the final stages of production, such as packaging and distribution, the machines are used to transport the finished barley powder to packaging lines, ensuring that the product reaches the market in a consistent and high-quality state. The versatility of these machines allows them to be integrated into existing production lines with minimal modifications, making them a practical choice for both new and existing facilities. By streamlining the powder handling process, these machines contribute to overall operational efficiency and help in reducing downtime and waste in barley processing operations.
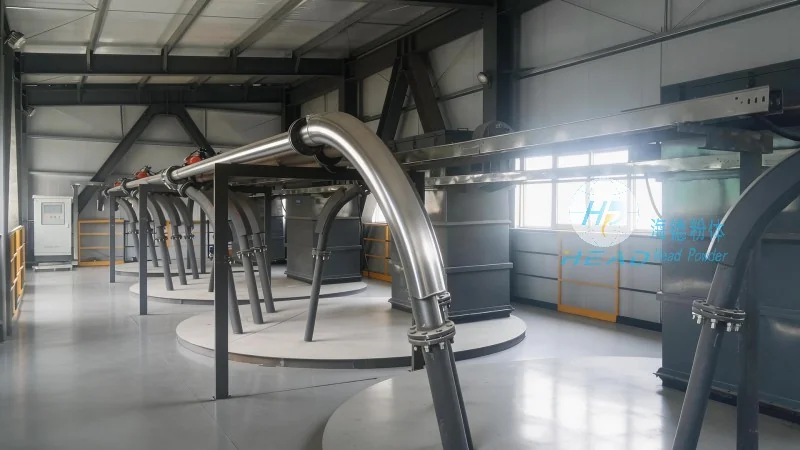
Maintenance and Operational Considerations
Proper maintenance and operational considerations are crucial for maximizing the lifespan and performance of barley powder conveying machines. Regular maintenance activities include cleaning the conveyor belts or screws to remove accumulated powder, inspecting for wear and tear on components, and checking the functionality of the control systems. It is important to use appropriate cleaning agents and tools to avoid damaging the equipment's surfaces. Additionally, operators should monitor the machine's performance regularly, checking for signs of clogging, excessive vibration, or abnormal noise, which may indicate a problem that needs to be addressed promptly. The use of high-quality spare parts from the manufacturer is recommended to ensure compatibility and maintain the machine's performance standards. Operational considerations also include training operators on the proper use of the machine and adhering to safety guidelines to prevent accidents. By following these maintenance and operational practices, businesses can ensure that their barley powder conveying machines operate efficiently and reliably, minimizing downtime and maximizing productivity.
Conclusion
In conclusion, barley powder conveying machines are essential equipment for the efficient handling and transportation of barley powder in industrial applications. The design principles, materials, and features of these machines are carefully engineered to address the unique challenges of handling barley powder, ensuring consistent performance and product quality. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced and reliable powder handling solutions that meet the needs of the barley processing industry. By investing in high-quality conveying machines and adhering to proper maintenance practices, businesses can enhance their operational efficiency, reduce costs, and maintain a competitive edge in the market. The continued development of these machines will likely lead to further improvements in performance and functionality, making them even more valuable in the future of barley processing and related industries.




