

What is an Automatic Powder Conveying System Equipment? What are its Design Principles?
For industries dealing with bulk powders, the efficiency and reliability of material handling systems are critical. An automatic powder conveying system equipment is a specialized solution designed to transport powders and granules from one location to another with minimal human intervention. This system is integral to processes in pharmaceuticals, food processing, chemical manufacturing, and other sectors where precise and consistent material movement is essential.
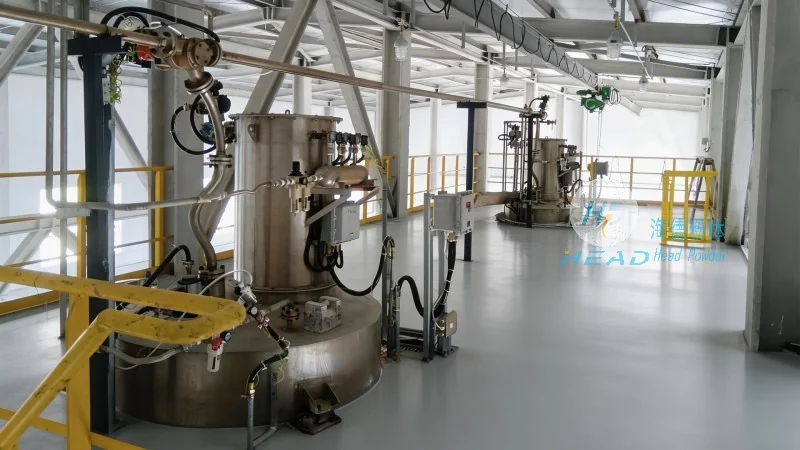
Introduction to Automatic Powder Conveying Systems
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and manufacturing of advanced powder handling solutions. Our company, often referred to as HeadPowder, has been a leader in providing innovative equipment tailored to the unique needs of various industries. The automatic powder conveying system is a sophisticated piece of machinery that integrates multiple components to ensure smooth, controlled, and safe powder transport. This equipment is engineered to handle a wide range of powder types, from fine powders to bulk materials, while maintaining the integrity and quality of the product.
Key Components of an Automatic Powder Conveying System
The design of an automatic powder conveying system involves several key components that work in harmony to achieve efficient material transport. These components typically include a hopper for material storage, a feeder to regulate the flow of powder, a conveyor mechanism (such as a screw conveyor, pneumatic conveyor, or belt conveyor), and control systems to monitor and adjust the process. The hopper is designed to hold the bulk material and ensure a consistent feed to the feeder. The feeder, often a rotary valve or a screw feeder, controls the rate at which powder is released into the conveyor system. The conveyor mechanism then transports the powder to the desired destination, such as a processing unit or a storage silo. Control systems, including sensors and programmable logic controllers (PLCs), are integrated to monitor parameters like flow rate, pressure, and temperature, ensuring optimal performance and preventing issues like clogging or overloading.
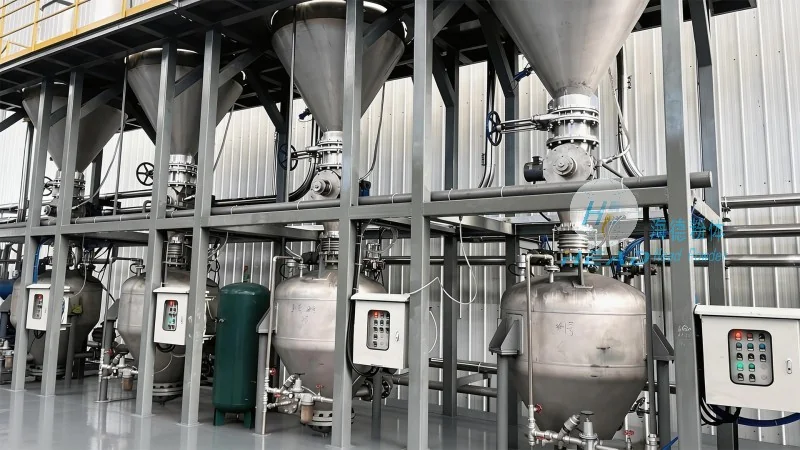
Design Principles and Engineering Considerations
The design principles of an automatic powder conveying system are centered on efficiency, safety, and adaptability. Engineers at HeadPowder consider several factors when designing these systems, including the physical properties of the powder (e.g., particle size, moisture content, flowability), the required conveying capacity, and the environmental conditions of the operation. The system must be designed to minimize product degradation, prevent contamination, and ensure compliance with industry standards and regulations. For example, in pharmaceutical applications, the equipment must be constructed from materials that are easy to clean and sterilize, and the conveying process must be sterile to avoid cross-contamination. In chemical manufacturing, the system may need to handle corrosive or hazardous materials, requiring specialized materials like stainless steel or explosion-proof components.
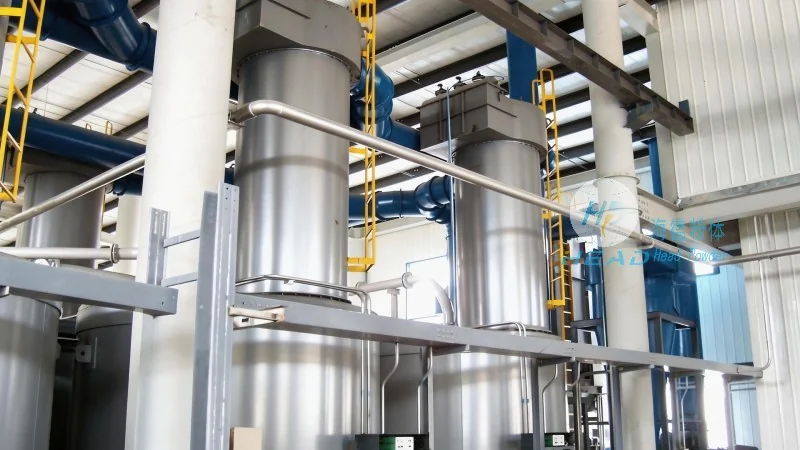
Advantages of Using Automatic Powder Conveying Systems
Implementing an automatic powder conveying system offers numerous advantages over traditional manual or semi-automated methods. Firstly, it significantly improves operational efficiency by reducing the time and labor required for material handling. The automated control systems ensure consistent and reliable performance, minimizing downtime and maintenance costs. Secondly, the system enhances safety by eliminating the need for manual handling of powders, which can be dusty or contain hazardous substances. This reduces the risk of respiratory issues or other health hazards for workers. Thirdly, the precision of the conveying process ensures that the correct amount of material is delivered to the next stage of production, improving product quality and reducing waste. Additionally, the system can be integrated with other production equipment, creating a seamless workflow that enhances overall productivity.
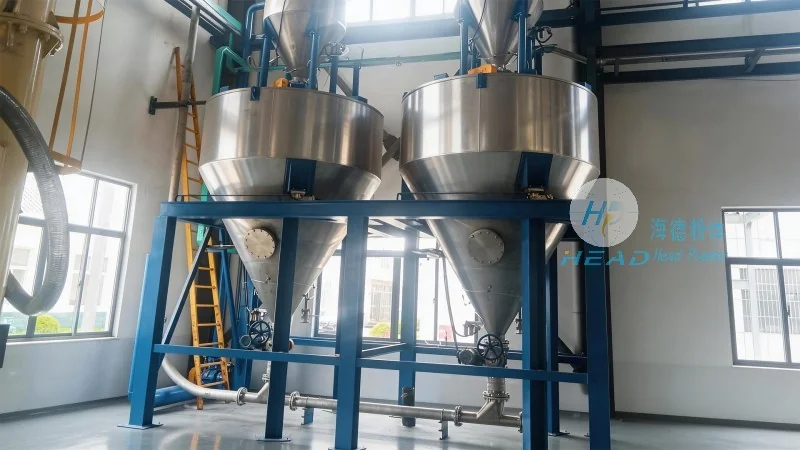
Customization and Application Flexibility
HeadPowder understands that different industries have unique requirements, and our automatic powder conveying systems are designed to be customizable. We offer a range of solutions tailored to specific applications, from small-scale laboratory setups to large-scale industrial production lines. Our engineers work closely with clients to assess their needs and design a system that meets their exact specifications. Whether the application involves high-speed conveying for food processing or low-speed, gentle handling for sensitive pharmaceutical powders, our equipment can be adapted to suit the requirements. The flexibility of our systems allows for easy integration with existing infrastructure and the ability to scale up or down as production needs change.
Conclusion
An automatic powder conveying system equipment is a vital component in modern industrial operations, providing efficient, safe, and reliable material handling solutions. At Shandong HeadPowder Engineering Co., Ltd., we are committed to delivering high-quality, innovative equipment that meets the diverse needs of our clients. Our focus on design principles, customization, and performance ensures that our systems not only meet but exceed industry standards. By investing in an automatic powder conveying system, businesses can enhance their operational efficiency, improve product quality, and ensure a safer working environment. As a leader in the field, HeadPowder continues to advance the technology of powder handling, providing solutions that drive success in various industries.