

Principle of Coffee Bean Pneumatic Conveying System
The coffee bean pneumatic conveying system is a sophisticated technology designed to efficiently transport coffee beans from one location to another within processing facilities. This system operates by using air as the medium to move the beans through a network of pipes or ducts. The fundamental principle involves creating a pressure differential that propels the coffee beans forward, ensuring a smooth and continuous flow. By leveraging pneumatic forces, the system minimizes the need for mechanical components like conveyors or elevators, which can be prone to wear and maintenance issues. This approach not only enhances operational efficiency but also preserves the quality of the coffee beans by reducing physical stress during transport.
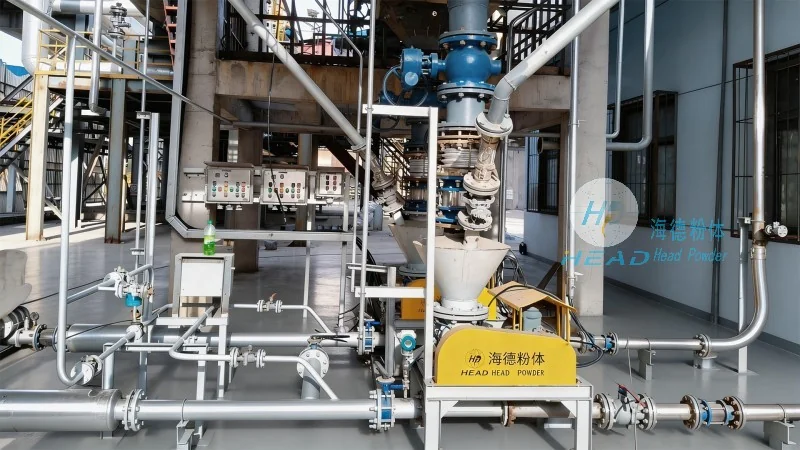
Key Components and Operational Mechanism
The coffee bean pneumatic conveying system consists of several critical components that work in tandem to achieve effective material handling. The primary elements include a hopper for loading the coffee beans, a blower or air compressor to generate the necessary air pressure, a pipeline network for transporting the beans, and a receiver or discharge point where the beans are collected. The hopper is typically equipped with a feeder that controls the flow of beans into the system. The blower creates a low-pressure zone at the discharge end, which draws the beans into the pipeline as they are carried by the moving air stream. This process, known as dilute-phase or dense-phase conveying, depends on the air velocity and the particle size of the coffee beans. Dilute-phase conveying uses higher air velocities to suspend the beans in the air, while dense-phase conveying uses lower velocities to move the beans in a more compacted form, reducing the risk of product degradation.
Advantages of Pneumatic Conveying in Coffee Processing
Implementing a pneumatic conveying system in coffee processing offers numerous advantages over traditional mechanical methods. One of the most significant benefits is the ability to maintain the integrity of the coffee beans. Unlike belt or screw conveyors, which can cause friction and abrasion, pneumatic systems minimize physical contact, preserving the bean's texture and flavor profile. Additionally, this technology allows for a more hygienic and clean environment, as the system can be designed with enclosed pipes and easy-to-clean components, reducing the risk of contamination. The flexibility of the system is another key advantage; it can be easily reconfigured to accommodate changes in production volume or layout, making it adaptable to varying operational needs. Furthermore, the system can integrate with other processing equipment, such as roasters or sorters, creating a seamless workflow that enhances overall productivity.
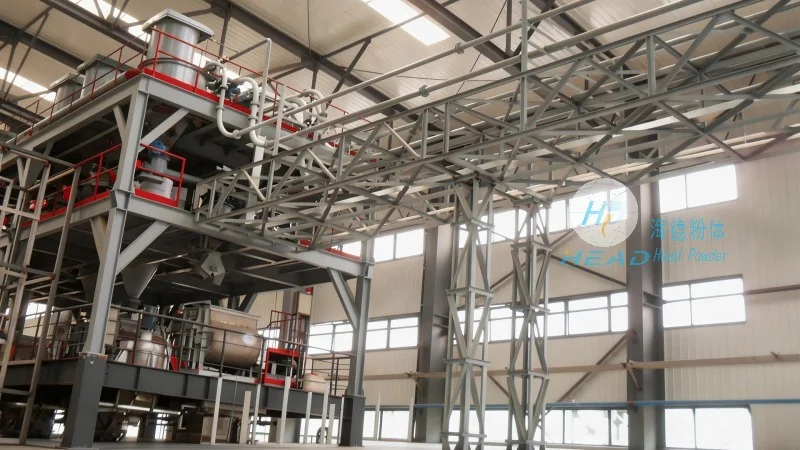
HeadPowder Engineering: Expertise in Coffee Bean Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and supplying advanced pneumatic conveying systems tailored to the coffee industry. With years of experience and a deep understanding of coffee processing requirements, HeadPowder has developed innovative solutions that address the unique challenges of handling coffee beans. The company's team of engineers leverages cutting-edge technology and industry best practices to create customized systems that meet the specific needs of each client. HeadPowder's commitment to quality is evident in its use of high-grade materials and rigorous testing protocols, ensuring that every system delivered is reliable and durable. The company's facilities in Shandong, China, provide a robust manufacturing base, enabling efficient production and timely delivery of products. By partnering with HeadPowder, coffee processing facilities can benefit from optimized material handling, reduced operational costs, and improved product quality.
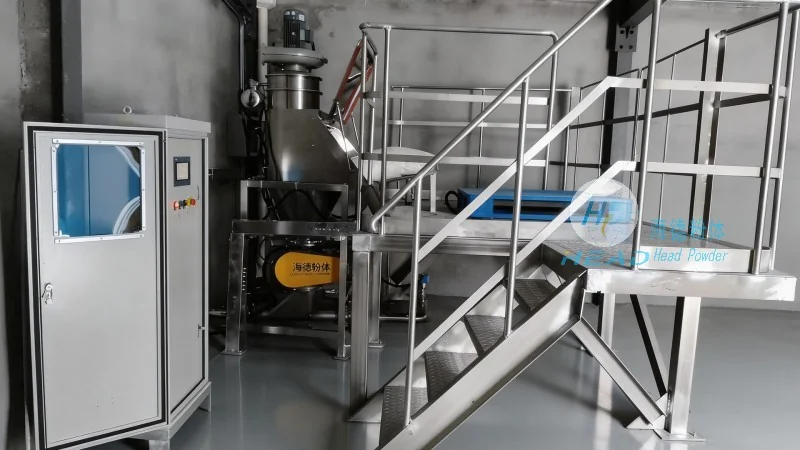
Customization and Integration for Optimal Performance
HeadPowder Engineering understands that each coffee processing operation has distinct requirements, which is why they offer comprehensive customization options for their pneumatic conveying systems. Clients can choose from various configurations, including dilute-phase or dense-phase systems, based on their specific production scale and product characteristics. The company also provides integration services to ensure that the conveying system works seamlessly with existing equipment, such as roasters, sorters, and packaging machines. This integration minimizes downtime and streamlines the overall processing workflow. HeadPowder's technical support team offers guidance throughout the entire process, from initial consultation and system design to installation and maintenance. This comprehensive approach ensures that clients receive a solution that not only meets their current needs but also supports future growth and expansion. By focusing on customization and integration, HeadPowder helps coffee processing facilities achieve optimal performance and maximize their operational efficiency.
Conclusion: Enhancing Coffee Processing with Pneumatic Conveying
In conclusion, the coffee bean pneumatic conveying system represents a significant advancement in material handling technology for the coffee industry. By leveraging air as the primary transport medium, this system offers numerous benefits, including improved product quality, enhanced hygiene, and operational flexibility. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing advanced pneumatic conveying solutions tailored to the coffee sector. With their expertise and commitment to quality, HeadPowder helps coffee processing facilities optimize their operations and achieve sustainable growth. As the demand for high-quality coffee products continues to rise, the adoption of efficient and reliable conveying systems like those offered by HeadPowder will play a crucial role in meeting industry standards and customer expectations.